


At Günay Heat Exchangers, we work to protect natural resources and build a sustainable future. We focus on using eco-friendly practices and maximizing energy efficiency to reduce our impact on the environment. We aim to meet future needs today and add value to society and the environment, ensuring a sustainable life for future generations

About Us
Innovative Cooling Solutions Offering High Efficiency
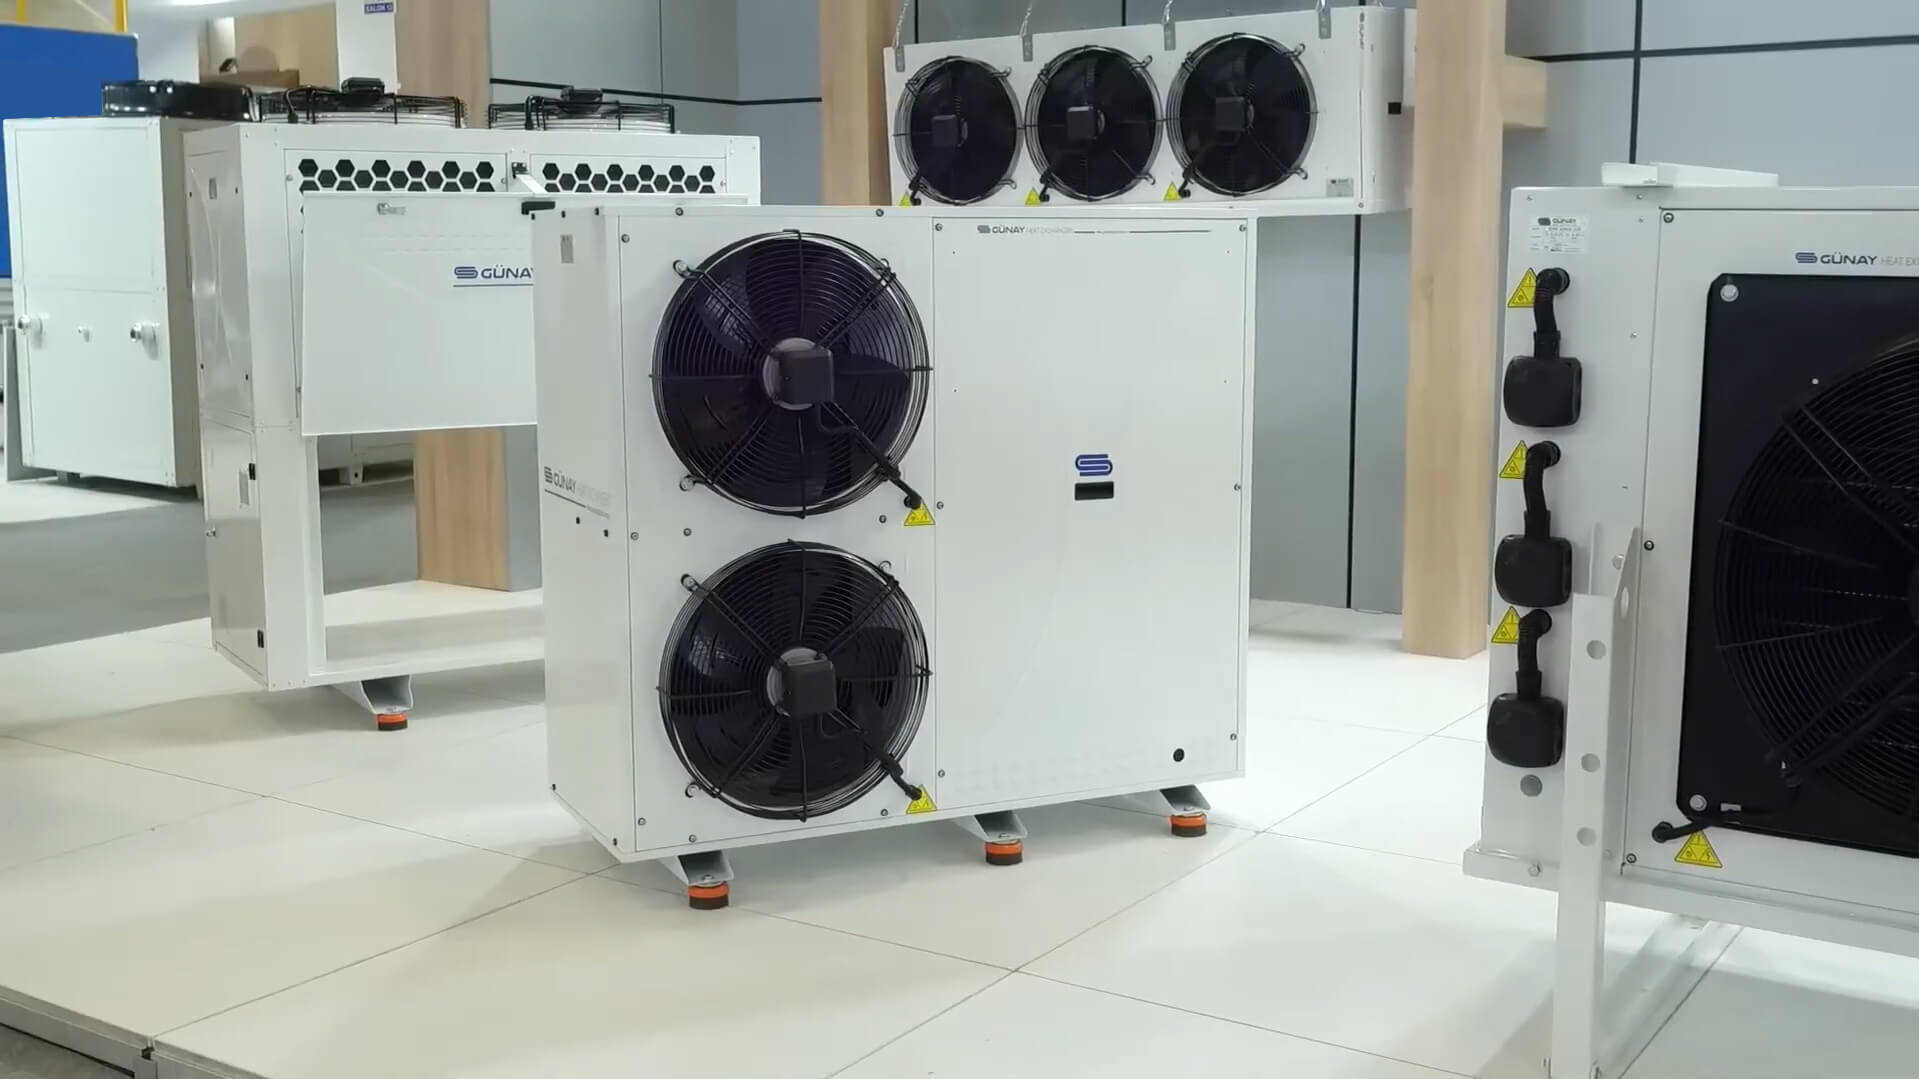
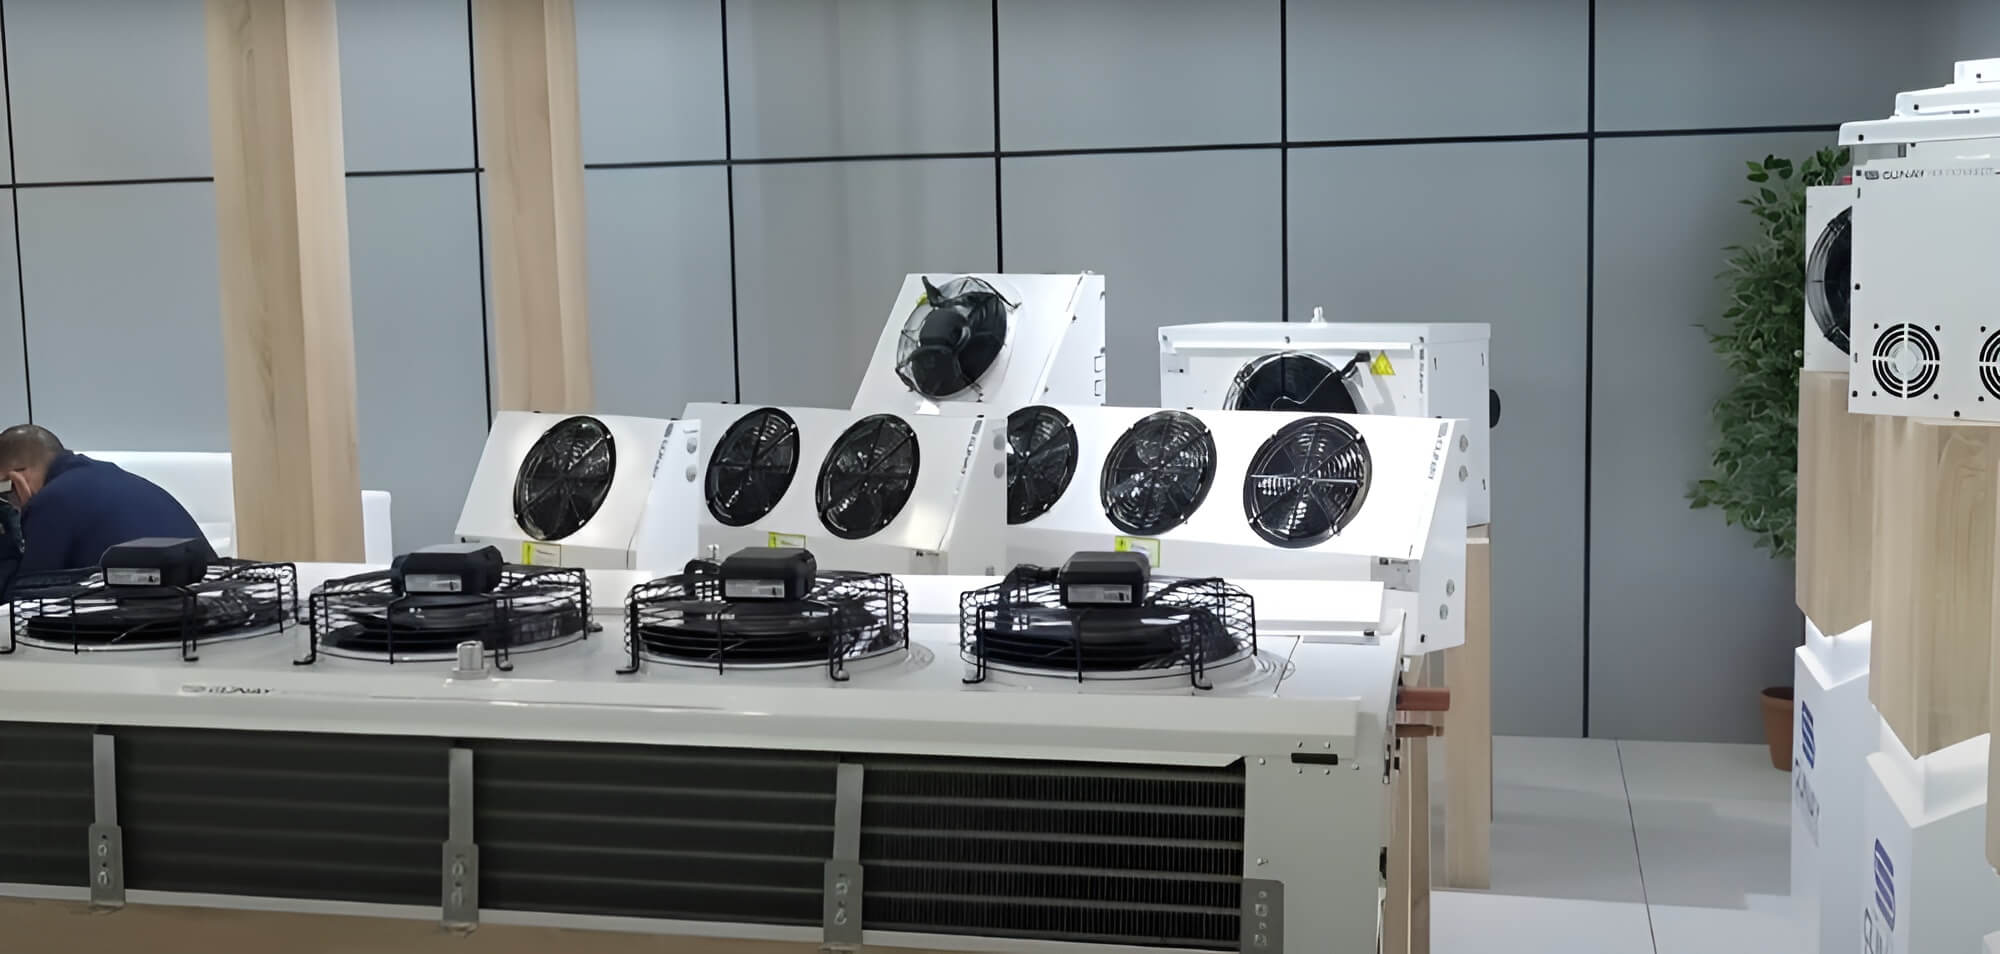
Since its establishment in 1986, our company has been offering evaporators, condensers, and heat exchangers both in mass production and as custom-made. Embracing both traditional and modern service approaches, Günay Heat Exchangers continues to evolve by constantly updating its infrastructure in line with industry innovations and customer expectations.
40
+ Years of Trust and Experience 
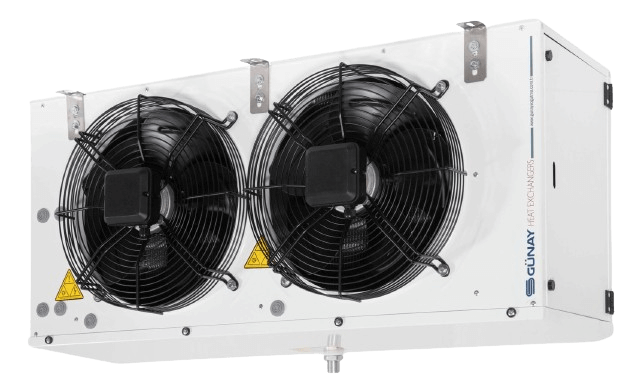
Evaporators
An evaporator is an essential component of cooling systems. Typically designed as a serpentine coil, it enables the refrigerant to evaporate and absorb heat from the surrounding environment. During this process, heat is transferred from the surroundings, thereby lowering the ambient temperature and achieving the desired cooling effect.
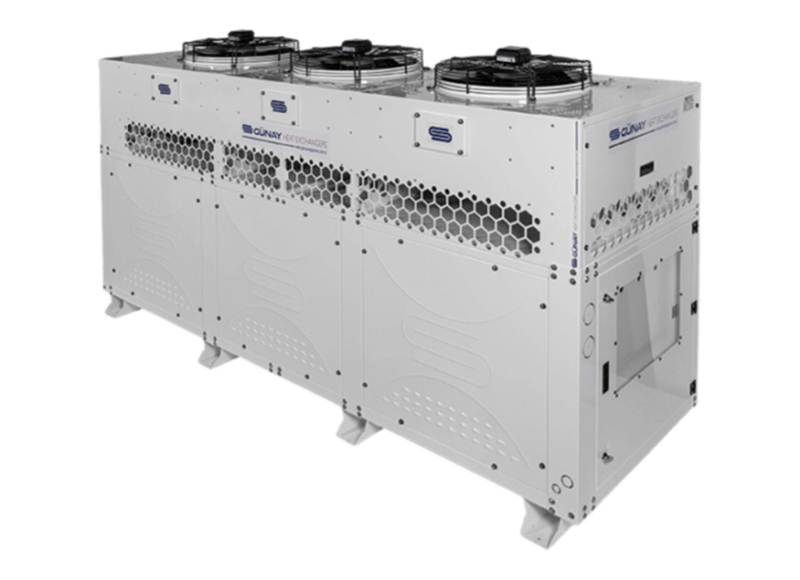
Condensers
The main function of a condenser is to condense the refrigerant gas into a liquid in the cooling cycle. During this process, the heat from the refrigerant gas is released to the surroundings, and the refrigerant condenses into a liquid form.
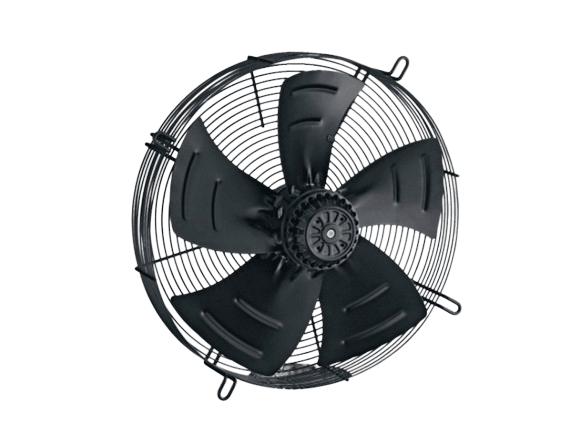
Axial Fans
Axial fans are designed to provide high airflow and play a critical role in industrial cooling solutions. These fans, which move air forward along the axis of the fan blades, are known for delivering high-volume airflow at low pressure. Thanks to these characteristics, they are an ideal solution for applications such as ventilating, cooling, or heating large areas.
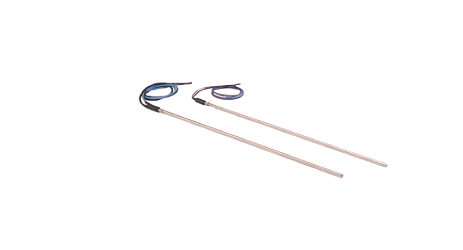
Resistances
Defrost is the process of melting frost and ice that accumulate on the surfaces of air coolers. In cold storage rooms, industrial kitchen sections, and similar areas where defrosting is needed, heaters provide suitable solutions for various heating requirements with different size and power options.
We Are With You Every Step of the Way
Safe Choice
0
+
Export to Countries
0
%
Customer Satisfaction
0
+
Employees
Contact us
Branches
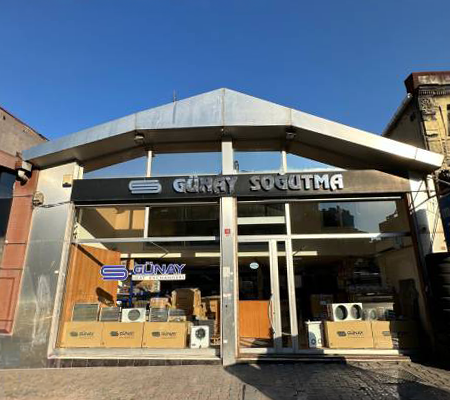
Istanbul Branch
Kocatepe Mahallesi Irmak Cad. No:43-45 Beyoğlu Dolapdere/İstanbul
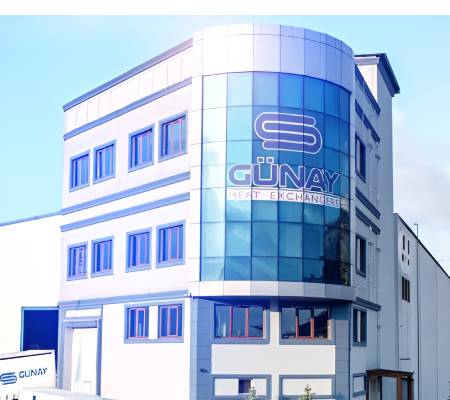
Factory
Yassıören Mahallesi Akpınar Sanayi Bölgesi Fırat Sokak No:6/1 Hadımköy-Arnavutköy/İstanbul
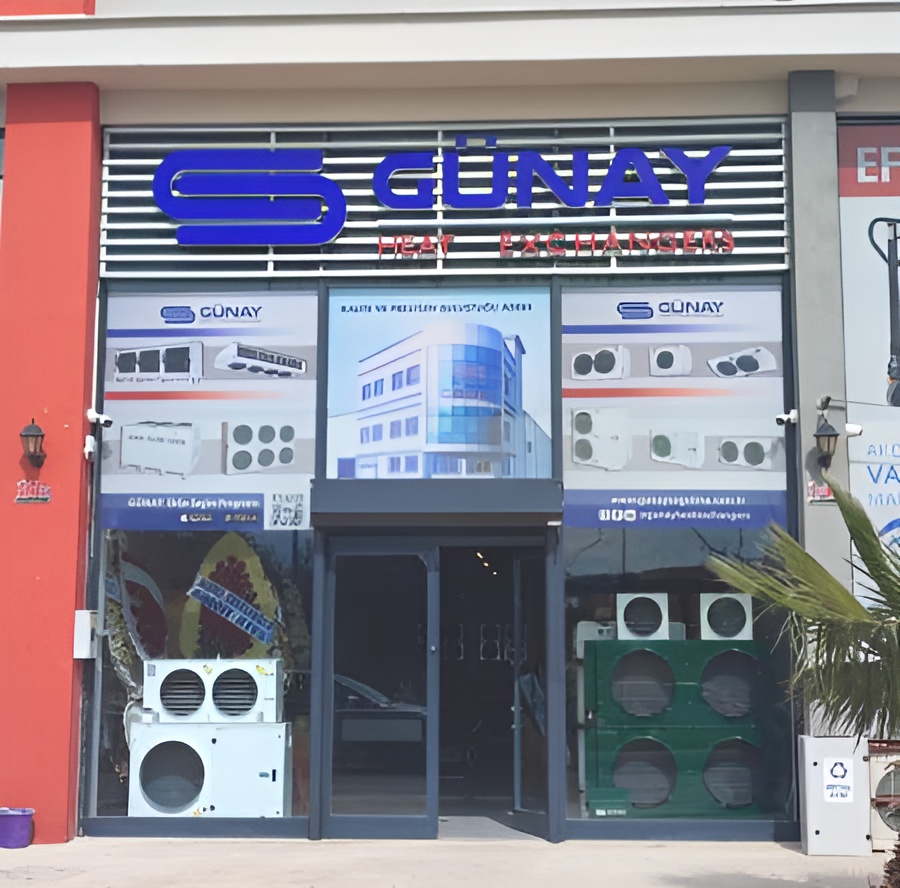
Antalya Branch
Beşkonaklılar Mahallesi Kırçiçeği Caddesi No:13E Corner City Plaza Kepez/Antalya
Izmir Branch
Barbaros Burak Reis Caddesi No:112 D:A, 35090 Bornova/İzmir
Günay Academy
Education Workshop


For More
Follow the Agenda
Blog
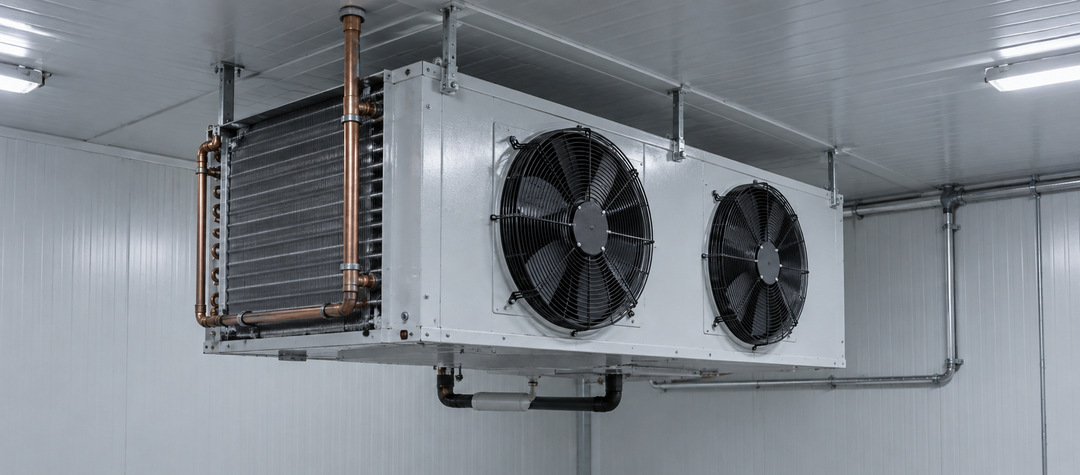
When you see a figure such as "5.0 kW" in an evaporator catalogue, it does not mean the unit will deliver 5.0 kW of cooling in every cold room. A catalogue capacity is a reference value defined for a specific air inlet temperature, evaporating temperature, relative humidity, refrigerant and fan condition. Operate the same unit at a different room temperature, with a different refrigerant or at a different temperature difference, and its capacity changes significantly. Selecting equipment without understanding these conditions can leave a cold room unable to reach its set point, lead to oversized and unnecessarily expensive equipment, or cause stored products to dry out. This guide explains, step by step, how to read catalogue capacities, which standards they are based on and how to adapt them to your own project. It is written for project engineers, refrigeration contractors, mechanical installation companies and technical purchasing managers. Table Of Contents What Exactly Does The Capacity In An Evaporator Catalogue Show? What Does The EN 328 Standard Define For Capacity Rating? What Are The SC1, SC2, SC3 And SC4 Standard Conditions? How Does DT1 Affect Evaporator Capacity? What Is The Difference Between Dry And Wet Capacity? How Does The Refrigerant Type Change Catalogue Capacity? How Do Fans, Power Supply And Airflow Affect Capacity? How Do Frost, Fouling And Installation Reduce Capacity On Site? How Do You Adapt A Catalogue Value To Your Own Project? How Do You Compare Catalogues From Different Manufacturers Correctly? How Should Capacity Data In Günay Catalogues Be Read? Frequently Asked Questions What Exactly Does The Capacity In An Evaporator Catalogue Show? Evaporator capacity is the amount of heat the unit can remove from the cold room air over a given period, usually expressed in watts (W) or kilowatts (kW). However, it is not a fixed property of the unit. Capacity depends on design features such as coil surface area, tube and fin geometry and airflow, but it also depends directly on the conditions in which the unit operates. That is why manufacturers always state capacity together with a reference condition. The number in the catalogue is shorthand for a longer sentence: "the stated evaporator removes the stated amount of heat at the stated air temperature, at the stated evaporating temperature, with the stated refrigerant and with the stated fan." Looking only at the number without reading the conditions is like comparing two prices without checking the currency. To interpret a catalogue capacity correctly, you need answers to four questions: For which air inlet temperature and which evaporating temperature is the capacity given? Is the value calculated for dry or for humid (wet) conditions? Which refrigerant is used as the reference? Which fan, which speed and which power supply are assumed? What Does The EN 328 Standard Define For Capacity Rating? In Europe and in markets that follow European standards, the performance of forced convection unit air coolers, in other words fan-assisted evaporators, is defined according to EN 328. The standard sets out the test method and the standard conditions under which the capacity of these units is determined. Such alignment allows products from different manufacturers to be compared against the same reference point. The standard fixes parameters such as air inlet temperature, evaporating temperature, relative humidity and superheat at specific values. When a manufacturer states "according to EN 328" in its catalogue, it indicates that the capacity is given for one of these standard conditions. There is one distinction worth noting. Some manufacturers determine capacity with calculation software based on EN 328 conditions, while others have their products tested and certified by independent laboratories. Both approaches refer to EN 328 conditions. Knowing how a value was obtained gives decision makers additional assurance when comparing catalogues, particularly on large projects. What Are The SC1, SC2, SC3 And SC4 Standard Conditions? EN 328 defines standard conditions, referred to as "SC", for evaporators operating with refrigerants. The four most widely used conditions are shown in the table below: Standard ConditionAir Inlet TemperatureEvaporating TemperatureDT1Relative HumidityTypical Application SC1 +10 °C 0 °C 10 K 85% Air-conditioned processing areas, high temperature storage SC2 0 °C -8 °C 8 K 85% Fresh produce storage, chilled cold rooms SC3 -18 °C -25 °C 7 K 95% Frozen product storage SC4 -25 °C -31 °C 6 K 95% Deep frozen storage The table also reveals the most common mistake made when reading catalogues. The capacity of the same evaporator at SC1 is much higher than its capacity at SC3. At low temperatures, the air carries less heat, the DT1 difference is smaller and the coil works under more demanding conditions. For example, looking at the SC1 capacity when selecting equipment for a freezer room running at -20 °C will make the unit appear far more powerful than it really is. For sub-zero applications, SC3 or SC4 values provide a more realistic starting point, while SC2 is more appropriate for chilled cold rooms. How Does DT1 Affect Evaporator Capacity? DT1 is the difference between the temperature of the air entering the evaporator and the evaporating temperature of the refrigerant. Expressed as a formula: DT1 = Air inlet temperature − Evaporating temperature. That difference is one of the most important factors determining how much heat the coil can remove from the air. For refrigerants with no glide or only a small glide, capacity is generally accepted to vary roughly in proportion to DT1. A hypothetical example illustrates the point: Assume an evaporator has a capacity of 5.0 kW at SC2 (DT1 = 8 K). If the same unit operates at a similar room temperature with DT1 = 6 K, its capacity will be approximately 5.0 × 6 / 8 = 3.75 kW. At DT1 = 10 K, capacity rises to approximately 6.25 kW. Such a calculation is a pre-selection tool; for a definitive result, the manufacturer's selection software or correction tables should be used. Even so, the example clearly shows why DT1 matters so much. DT1 affects not only capacity but also humidity inside the room. A higher DT1 allows the same capacity to be achieved with a smaller evaporator, but more of the moisture in the air condenses and freezes on the coil. That effect lowers the relative humidity in the room, increases moisture loss from unpackaged products and leads to more frequent defrosting. Lower DT1 values are usually preferred for moisture-sensitive products such as fruit, vegetables and unwrapped meat. For packaged products, operating with a higher DT1 can be an economical option. What Is The Difference Between Dry And Wet Capacity? When an evaporator cools air, it removes two types of heat. The first is sensible heat, which lowers the air temperature. The second is latent heat, released when moisture in the air condenses or freezes on the coil. Dry capacity accounts only for sensible heat, while wet capacity also includes the moisture load. That distinction matters most at positive temperatures. Based on coefficients commonly used in the industry, wet capacity at SC1 can be noticeably higher than dry capacity, by roughly one third. At SC2 the difference is smaller. At low temperatures such as SC3 and SC4, the air holds very little moisture, so dry and wet capacities are very close to each other. In practice, the consequence is that if one catalogue gives wet capacity and another gives dry capacity, you will see different figures even for units of the same size. Always check the footnotes or technical notes of a catalogue to see which humidity condition the capacity is based on. How Does The Refrigerant Type Change Catalogue Capacity? Catalogue capacities are usually given for a single reference refrigerant. For many years that reference has been R404A, and many manufacturers' catalogues are still based on R404A values. When a different refrigerant is used, its thermodynamic properties differ, so the capacity changes as well. The difference appears in two ways: Heat transfer properties of the refrigerant: Under the same conditions, some refrigerants deliver slightly lower capacity than R404A. Manufacturers show that difference through refrigerant-specific correction factors. Temperature glide: In refrigerant blends, evaporation does not take place at a single temperature but across a temperature range. In such cases, whether "evaporating temperature" refers to the mean temperature or to the dew point directly affects the calculated capacity. If your project will use a refrigerant other than R404A, the safest approach is to ask the manufacturer for a selection carried out for that refrigerant, rather than using the catalogue value directly. With refrigerant transitions accelerating, such verification has become especially important when upgrading existing facilities. How Do Fans, Power Supply And Airflow Affect Capacity? In a fan-assisted evaporator, capacity is directly linked to the volume of air passing through the coil. Catalogue values are calculated on the assumption of a specific fan model, fan diameter, speed and power supply. If any of those assumptions change, airflow changes, and so does capacity. Common situations on site include: A different fan model: If a fan with different characteristics replaces the one specified in the catalogue, airflow and pressure change. A different mains frequency: When a unit rated for 50 Hz operates on a 60 Hz supply, fan speed changes. Such a shift affects airflow, sound level and motor load. Speed control: Reducing fan speed can bring energy and noise benefits, but capacity decreases accordingly. Obstructions in the air path: Racks, pallets or air ducts increase the resistance the fan must overcome, pushing actual airflow below the catalogue value. Air throw is usually listed separately in the catalogue. Even if capacity is sufficient, warm spots will form if the air cannot reach the far corners of the room, and product temperatures will become uneven. How Do Frost, Fouling And Installation Reduce Capacity On Site? Catalogue values apply to a clean coil under standard laboratory conditions. Actual capacity on site can fall below that value over time for several reasons. Frost build-up: At sub-zero temperatures, the layer of frost that forms on the fins narrows the air passages and weakens heat transfer. The longer the interval between defrosts, the greater the capacity loss. Fouling and dust: Particularly in processing areas, dirt and grease that accumulate on the fins effectively reduce the heat transfer surface of the coil. Incorrect positioning: Placing an evaporator above a door, installing it with the suction side too close to a wall, or allowing racks to interrupt airflow prevents the unit from delivering its catalogue capacity. Piping and adjustment errors: An incorrectly set expansion valve, insufficient refrigerant charge or unsuitable pipe sizes reduce evaporator efficiency. For that reason, selection should not aim merely for "enough" capacity but should include a safety margin suited to operating conditions. The size of that margin should depend on the product type, door opening frequency and defrost strategy. How Do You Adapt A Catalogue Value To Your Own Project? The following steps can be used to adapt a catalogue capacity to a project: Determine the heat load: Calculate the total cooling requirement based on room dimensions, insulation, product quantity and entry temperature, door openings, lighting and personnel. Define room temperature and target humidity: The stored product determines the required relative humidity and a suitable DT1 range. Set the evaporating temperature: Subtract the selected DT1 from the room temperature to find the evaporating temperature. Choose the closest standard condition: Use the SC condition that best matches your application as a reference. Apply corrections: Use the manufacturer's correction factors for DT1, refrigerant, dry or wet capacity and fan conditions. Add a safety margin: Leave a reasonable margin for frost, fouling and operational uncertainty. Verify the selection: Where possible, check the result with the manufacturer's selection program or technical team. These steps significantly reduce the risk of incorrect selection, especially in projects where several evaporators serve the same room or where custom-sized units are required. How Do You Compare Catalogues From Different Manufacturers Correctly? The most common mistake in purchasing is placing capacity values from different catalogues side by side without checking their conditions. The checklist below supports a fair comparison: CheckpointWhy It Matters Standard condition (SC1, SC2, SC3, SC4) Capacities given under different conditions cannot be compared directly. DT1 value Capacity changes roughly in proportion to DT1. Dry or wet capacity At positive temperatures, the difference can be large. Reference refrigerant Different refrigerants deliver different capacities. Fan model, speed and power supply Airflow directly affects capacity. Coil surface area and fin spacing These determine long-term performance and frosting behaviour. Air throw Shows whether uniform cooling will be achieved across the room. How the capacity was obtained Calculated and independently tested values offer different levels of assurance. If even one of these criteria differs, the capacity gap between two quotations may not reflect a real performance difference. For technical purchasing managers, the most practical approach is to ask every supplier to make a selection based on the same project conditions. How Should Capacity Data In Günay Catalogues Be Read? Since 1986, Günay Heat Exchangers has supplied evaporators, condensers and heat exchangers in both serial and custom production. The technical data for evaporator series such as the GNA and GND commercial types, the GNE standard type and the GNI industrial type state that capacities are calculated in accordance with EN 328 standards for R404A, based on European fans. This means you should pay attention to the following when reading Günay catalogues: Check which standard condition (SC) the capacity in the model table refers to. If your project uses a refrigerant other than R404A, ask the Günay technical team for a refrigerant-specific evaluation. If you plan to request a different fan model, clarify its effect on capacity during selection. Optional fan model changes can be applied to Günay products. Choose the fin spacing that suits your room temperature. The GNE series, for example, offers fin spacing options of 4, 6, 8 and 10 mm. Günay's product selection program helps you select evaporators, condensers and heat exchangers based on your project data. Where non-standard dimensions, special refrigerants or demanding ambient conditions are involved, a custom production option allows an application-specific solution to be developed. Technical support and quotations are available through the Istanbul, Antalya and Izmir branches and the factory in Arnavutköy, Istanbul. Frequently Asked Questions Why Is Capacity On Site Lower Than The Catalogue Value? Catalogue values are given for a clean coil, standard air and evaporating temperatures, a specific fan and a reference refrigerant. A lower DT1 on site, frost, fouling, racks obstructing airflow or the use of a different refrigerant can all push capacity below the catalogue value. Which Standard Condition Should I Use For A Freezer Room? For frozen storage rooms at around -18 °C, SC3 provides a more realistic reference, and SC4 is more suitable for deep freeze applications at lower temperatures. Selecting a unit for a freezer room based on SC1 or SC2 values overstates its capacity. Is A Higher DT1 Always An Advantage? No. A higher DT1 allows the same capacity to be reached with a smaller evaporator, but it lowers room humidity, increases moisture loss from products and requires more frequent defrosting. For moisture-sensitive products, a lower DT1 is usually the better choice. Are Condenser Capacities Also Given Under Similar Conditions? Yes, standard conditions are also defined for air-cooled condensers. Condenser capacity is usually given for the difference between the air inlet temperature and the condensing temperature, for example dT = 15 K. For Günay's GK series commercial condensers, capacities are calculated for R404A at dT = 15 K based on European fans. How Can I Make Capacities In Different Quotations Comparable? The most reliable method is to send every supplier a single technical brief that includes the room temperature, evaporating temperature, refrigerant, heat load and ambient conditions, and to ask each of them for a selection based on those conditions. This way, quotations can be compared against the same reference point.
Read More
Why a Cooling System Is Never Just a Single Product When a cooling system is being set up, a single product is often what people look for: "an evaporator", "a condenser". Yet a system working in the field is never a single part — it is the coordinated operation of several pieces of equipment that absorb heat from the space, carry it, reject it outside and, when necessary, melt the ice. An evaporator used in a cold storage room and an evaporator used on a supermarket shelf work on the same principle, but their fin spacing, defrost method and capacity curve are designed completely differently. The same applies to the condenser, axial fan and heater. This article covers the technical framework needed to request the right equipment correctly when working with a cooling equipment supplier: what each type of equipment does, which combination works in which sector, and why a wrong match leads to inefficiency or failure. For an engineer or purchasing officer looking at Günay Heat Exchangers' product portfolio, this distinction is the first thing to be clarified before starting quotation talks with a supplier. The picture encountered in practice is this: the project owner knows the capacity value but has not clarified how this capacity will be shared among four different components. However powerful the evaporator is on its own, if the condenser opposite it cannot reject the heat fast enough, the system never reaches the expected temperature; if the fan airflow is insufficient, part of the evaporator surface is put out of use. Equipment selection is therefore an engineering decision that must be treated as a whole, not part by part. Evaporators: The Heat-Absorbing Side of the System The evaporator is the component of the cooling circuit that draws heat from the space. As the refrigerant passing through it evaporates, it absorbs heat from the surrounding air and the ambient temperature drops. Fin spacing, tube diameter and number of circuits vary with the target temperature range and humidity load. Evaporator Types and Sector-Specific Use Cold storage rooms: In rooms operating at low temperatures (-18°C and below), evaporators with wide fin spacing and electric or hot gas defrost are preferred; since frost can quickly cover the surface area, fin spacing is a critical design parameter. Supermarket and display shelf cooling applications: Evaporators used in shelf applications are designed to be more compact, low-noise and suited to frequent defrost cycles; since they operate close to the customer area, sound level is also taken into account in the design. Food processing and process lines: In environments with high humidity and frequent door openings, models with stainless steel coating and housings suitable for hygienic cleaning are used. Another parameter to look at when selecting an evaporator is the TD (temperature difference) value — the difference between the evaporator surface temperature and the room temperature. A low TD means less moisture is removed from the air (less drying of the stored product) and less frost, but it requires a larger evaporator surface; in projects with limited mechanical space, this creates a balancing problem. In applications with high humidity sensitivity such as food storage the TD is kept low, whereas in areas where dry goods are stored, a more compact evaporator with a higher TD may be preferred. For models with different circuit configurations, a selection can be made according to the application within the evaporator range. Condensers: The Point Where Heat Is Rejected The heat absorbed in the evaporator is pressurised through the compressor, carried to the condenser and rejected to the outside environment there. Condenser selection is directly related to the climate conditions and the machine room space. Air-Cooled and Water-Cooled Condenser Distinction Air-cooled condensers are preferred in rooftop or open-area installations and in industrial facilities where water supply is limited. Water-cooled systems, on the other hand, are used in large industrial facilities that require higher capacity density and have continuous cooling tower support. In export projects, the customer often shares the summer temperature average and humidity of their region; the condenser capacity calculation is revised according to this data. If the condenser is not selected with sufficient capacity, the condensing pressure rises, energy consumption increases and compressor life is shortened — for this reason condenser selection is generally not independent of the evaporator capacity but is calculated together with the evaporator load and compressor data. In industrial environments with heavy dust or dirt, keeping the condenser fin spacing wide also directly affects the cleaning interval and efficiency loss. For a model comparison according to the application, the condenser product group can be reviewed. Axial Fans: The Invisible Engineering of Airflow Axial fans are the component that provides airflow on both the evaporator and the condenser side; although their visibility is low, much of the system's efficiency passes through them. Blade angle, motor power and speed are determined according to the required airflow and the permitted noise level. Sector Differences in Fan Selection Supermarket/in-store applications: Low-speed, quiet fans are preferred because the equipment is close to the customer area. Cold storage rooms and industrial facilities: Since there is a higher airflow requirement, multi-blade fans that withstand high static pressure are used. Outdoor condenser units: Large-diameter, low-speed fans are preferred to ensure unobstructed airflow; in this way energy consumption is also kept under control. The number of fans is also not a value to be considered on its own; the same total airflow can be provided by several small fans instead of one large fan. Multi-fan arrangements allow the system, when one of the fans fails, not to stop completely but to keep running with part of its capacity — this redundancy is a reason for preference especially in cold storage rooms operating 24/7. Motor type selection likewise varies with the application; although fixed-speed motors are simple and low-cost, at part-load conditions fans with EC motors (electronically commutated) adjust their speed according to demand and save energy. For models in different airflow and noise classes, the axial fan range can be reviewed. Heaters: The Key to Defrost and Freeze Control Ice accumulating on the evaporator surface directly reduces heat transfer. For this reason, especially in systems operating below 0°C, electric heaters act as defrost — they switch on at certain intervals and melt the ice layer on the surface. Heater power and placement are calculated according to the evaporator's fin surface area and the ambient humidity load; a heater selected with insufficient power prolongs the defrost time, while one selected with excessive power leads to energy waste and local heat stress. For defrost heaters intended for different applications, the heater product group can be reviewed. How to Build the Right Equipment Combination Knowing the features of each piece of equipment individually is not enough; the real engineering decision is how these four components match each other. An evaporator of the same capacity can never reach the expected temperature if the condenser and fan placed next to it are insufficient. Cold Storage Room Combination Wide fin spacing evaporator + high-capacity air-cooled condenser + high-airflow axial fan + electric defrost heater. The priority here is being able to manage frost during long operating hours. Supermarket and Shelf Cooling Combination Compact evaporator + medium-capacity condenser + low-noise fan + frequent-cycle heater. The priority here is acoustic comfort and a fast response to frequent door openings. Food Processing Facility Combination Evaporator with a hygienic surface + condenser with high humidity tolerance + corrosion-resistant fan housing + strong defrost heater. A high humidity load directly increases defrost frequency. Industrial Facility and Process Cooling Combination Large-volume evaporator groups + high-capacity industrial-type air-cooled condenser units + multi-blade fan arrangement. In this segment the capacity is continuous, so the equipment is selected for uninterrupted load. Common Mistakes in Equipment Selection Selecting the condenser by catalogue rather than by climate: In regions with high ambient temperature or humidity, the catalogue capacity may not deliver the expected performance on site. Not calculating fan airflow according to the evaporator surface: Insufficient airflow causes part of the evaporator surface to work inefficiently. Selecting heater power with a fixed catalogue value: Every application has a different humidity load; using a fixed value either shortens the defrost time or prolongs it unnecessarily. Putting together components from different manufacturers on the assumption that "they will be compatible": Circuit calculations and pressure drop values differ between manufacturers; system integrity can be compromised. Increasing capacity without considering mechanical space constraints: When there is not enough installation space for an evaporator or condenser on site, increasing the number of units instead of increasing capacity (for example, two medium-sized evaporators instead of one large evaporator) can be a more feasible solution; if this assessment is not made at the project stage, revision is needed during site implementation. The Effect of Equipment Combination on Energy Consumption and Maintenance Frequency In a system that is not correctly matched, energy loss generally comes not from a single component but from the imbalance between components. For example, in a system with a condenser selected smaller than required, the compressor has to work at higher pressure and this permanently increases energy consumption — the source of the problem is not the compressor but the condenser-compressor match. Similarly, if the fan airflow is selected too low for the evaporator surface, dead zones form on the evaporator, these zones become more prone to frosting over time and the defrost heater has to switch on more often. The same logic applies on the maintenance side: in a system where capacity balance has been established between components, each part works within its own design range and wear becomes predictable. In an unbalanced combination, however, since one component constantly works at limit values, failure frequency increases and the maintenance schedule becomes unpredictable. The Importance of Equipment Variety for Exporters and OEM Manufacturers For OEM manufacturers exporting to the DACH region and Europe, equipment variety gains an extra dimension: within the same project, evaporators at different capacity steps, condensers suited to different climate conditions and fan selection compliant with local energy efficiency standards are requested together. Being able to source a wide product range from a single manufacturer reduces the compatibility risk between the components in the project and brings technical communication to a single point of contact. How Günay Heat Exchangers' Equipment Portfolio Comes Together With a manufacturing history of over 40 years, Günay Heat Exchangers produces its evaporator, condenser, axial fan and heater lines under one roof. This means a process that runs from capacity calculation to production in one hand, instead of four different components in a project being sourced from separate suppliers and harmonised on site. For projects in cold storage, supermarket cooling, food processing and industrial facilities, a selection can be made among the product groups according to different combination needs. Conclusion: The Right Combination Is the Foundation of an Efficient System The performance of a cooling system comes not from the quality of a single component but from how correctly the evaporator-condenser-fan-heater quartet is matched to each other. Starting equipment selection not by looking at the catalogue but by looking at the temperature, humidity and cycle needs of the sector to be served directly affects both energy consumption and failure frequency. Evaluating these four components together at the project stage costs far less than the cost of revision made later on site. Contact Us for the Right Equipment Combination for Your Project If you would like to evaluate the evaporator, condenser, axial fan and heater combination together for your cold storage, supermarket cooling, food processing or industrial facility project, our technical team can review your project details and suggest a suitable capacity match. You can reach us via our contact page. This content was updated on 22 September 2026.
Read More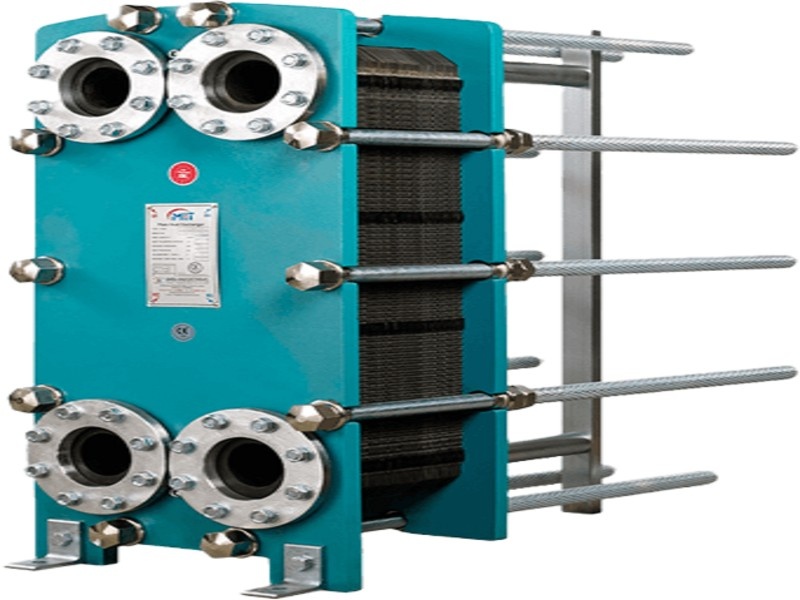
Choosing a Heat Exchanger Supplier: More Than a Price Quote Sitting down at the table with only a unit price and a lead time when choosing a heat exchanger supplier can turn into a costly mistake in the medium and long term. When it comes to an evaporator, a condenser or a custom-designed heat exchanger, the purchasing decision is really a decision about an engineering partnership. Choosing the wrong supplier results in incompatibility on site, revision delays, warranty disputes and ultimately a slipped project delivery date. Unlike the classic "what is a heat exchanger and how does it work" explanation, this article offers a concrete evaluation checklist that purchasing and engineering teams can use when shortlisting a supplier. The aim is to make the real capacity behind the quotation file visible and to move the decision process from intuition to measurable criteria. 1. Engineering and Design Support The difference between a supplier that sells a standard catalogue and one that evaluates your project's thermal load, fluid properties and installation constraints with you shows up in the first technical meeting. When assessing a supplier's engineering support, ask the following questions: Are thermal calculation and sizing done by an in-house team, or outsourced to a third party? What is the response time when a design revision is requested for a special fluid, pressure or temperature range? Is there technical staff who can adapt an existing product (for example evaporators) to your project? In the first meeting, are only prices asked about, or are questions asked about the application conditions (ambient temperature, fluid type, installation space)? A supplier with strong engineering support asks you questions before the quotation; it does not only answer your questions after the quotation. Why Is Design Flexibility So Important? In industrial cooling projects, site conditions almost never match the catalogue exactly. When it comes to a heat exchanger in custom dimensions for an OEM manufacturer, or a version that has to be retrofitted to an existing system, a supplier without design flexibility puts you in a bottleneck in the later stages of the project. 2. Technical Documentation and Drawing Support One of the most overlooked but most critical items in the purchasing process is documentation. Look not at a supplier's quotation file but at the quality of the documents it provides in the post-quotation process: Do dimensioned installation drawings (general arrangement drawing) come with the quotation, or after the order? Are material certificates and test reports provided on request? How quickly is an updated drawing delivered when a revision is requested? Is the maintenance and operation manual clear enough for the technical team on site to understand? Working with a supplier with weak documentation means the site team constantly making phone calls and creating email chains during installation and ultimately the work slowing down. A strong supplier sees documentation not as an after-sales chore but as a natural part of delivery. 3. Production Capacity and Flexibility A supplier's product range may look wide, but the real question is this: can it produce a volume like yours, in the time frame you want? Points to pay attention to when evaluating production capacity: Is there a separate production line or planning for standard products and custom orders? Can it show flexibility for urgent/priority orders, or does it process a single fixed queue? Is there an alternative supplier network for the main components in the supply chain (copper tube, aluminium fin, motor, compressor group, etc.), or is it dependent on a single source? How much does the lead time extend for large orders that require capacity increase? Looking at the product groups is a useful reference point for understanding whether a supplier produces in only a single equipment type or in a wide range from evaporators to axial fans. 4. Quality Control Processes "We have quality control" is meaningless on its own; what should be asked is at which stages and with which method this control is carried out. Ask a supplier to clarify the following details: Does quality control start at raw material intake, or is it applied only to the final product? At which stage and how are weld seams, pressure tests and leak-tightness checks documented? Are there intermediate control points on the production line, or is all control done at a single stage before shipment? Is transparent information shared about the rate of rejected or revised batches? The transparency of the quality control process is one of the clearest indicators of a supplier's corporate maturity. A supplier that cannot give a clear answer on this or brushes it off with generic statements may cause surprise costs on site. 5. Reference Projects and Industry Experience How many years a supplier has been in the industry is not a sufficient indicator on its own; what matters is whether it has experience in projects similar to your application area. During the evaluation, ask about the following: Can it provide a reference project for your sector (cold storage, industrial facility, HVAC application, etc.)? Can it provide information on how many years the equipment in the reference projects has been operating trouble-free in the field? Does it have an application history in demanding conditions (high humidity, corrosive environment, continuous duty)? Has it been able to build a repeat business relationship with the same customer — this is indirect proof of customer satisfaction. To get an idea of the company's general history, production philosophy and position in the sector, reviewing the supplier's corporate page helps you ask reference questions more accurately. 6. Delivery Reliability and Logistics Planning In industrial projects, a delay is not only the delay of a single piece of equipment but the slipping of the entire project schedule. When evaluating delivery reliability: How consistent is the lead time given at the quotation stage with the actual lead time? For international shipments, are customs processes and logistics coordination managed by the supplier? Is partial delivery or staged shipment offered? When a risk of delay arises, is proactive information given, or does the problem only surface when asked? This item is especially critical for an export-oriented supplier; the ability to coordinate between different customs regimes, transport times and certification requirements is the biggest determinant of delivery reliability. 7. After-Sales Support and Technical Service The supplier relationship does not end once the equipment is installed on site — the real test often begins here. Questions to ask when evaluating after-sales support: In case of a fault or performance problem, through which channel and within what time is technical support provided? Is there a separate stock policy for spare part supply? Is the warranty scope clearly defined, or limited to vague wording? Is remote technical consultancy or a site visit offered? The strength of after-sales support usually reveals whether a supplier is a long-term business partner or a one-time seller. 8. How to Audit a Supplier On Site If possible, visit the production facility of the supplier you have shortlisted or request a site tour via video. Points to observe during an audit: Are order and workflow in the production area logical, or chaotic? Where on the production line are the quality control stations located? The variety of ongoing orders (single type only, or are different sizes and custom-designed orders produced together)? What are the material storage conditions (protection against corrosion, correct labelling)? Are test equipment (pressure test unit, leak detector, etc.) up to date and regularly calibrated? An audit visit allows you to see how the claims in the quotation file match reality on the ground. Buyers who skip this step usually notice the problem after the equipment is commissioned. 9. Additional Criteria to Look for in Export-Oriented Suppliers For buyers working especially on projects aimed at the European market (particularly the DACH region), the following should also be evaluated in addition to the standard criteria: To which countries and at what volume does the supplier's export experience extend? Is there a practice of complying with the technical standards of different countries (voltage, connection type, certification language)? In which languages can technical documentation be provided in communication with international customers? What direction do past experiences in cross-border deliveries point to? Seeing which countries a supplier exports to regularly gives a concrete idea of how accustomed that supplier is to international standards. In this context, the export countries page is a practical starting point for buyers who want to understand the breadth of a supplier's geographic experience. 10. Building a Shortlist: A Scoring Approach When comparing several suppliers, converting the above criteria into a simple scoring table, instead of relying on intuition alone, makes the decision process objective. An example approach: Engineering/design support — weak / adequate / strong Documentation quality — weak / adequate / strong Production capacity and flexibility — weak / adequate / strong Quality control transparency — weak / adequate / strong Reference/experience fit — weak / adequate / strong Delivery reliability — weak / adequate / strong After-sales support — weak / adequate / strong Filling in this table after each quotation lets you move from a purchasing process that decides on price alone to one that can see risks in advance. Common Mistakes in the Evaluation Process Even experienced purchasing teams can fall into some recurring mistakes. Reviewing these points before building the shortlist prevents you from saying "we wish we had asked" at the end of the process: Comparing only the unit price: The difference between two quotations usually comes from differences in material thickness, coating type or test scope; price alone does not offer a meaningful comparison. Seeing the quotation file as the only source: A quotation file is a document in which the supplier describes itself in the best light. Decisions made without reference checks and site audits leave most of the risk invisible. Not asking about post-commissioning support: Compatibility problems that appear after the equipment is delivered may remain with the buyer if the warranty scope is not clear. Deciding after talking to only one person: The promises made by the sales representative and the capacity that the production/engineering team can actually offer may sometimes not match; if possible, request a direct meeting with the technical team. Most of these mistakes disappear on their own when a technical checklist is included in the evaluation process at an early stage. Summary: Quick Evaluation Checklist Does it ask technical questions before the quotation? Do the dimensioned drawing and documentation come with the quotation? Is there separate capacity planning for custom orders and standard production? Are the quality control stages clear and documentable? Can it offer a concrete reference project suited to your sector? Has the quoted lead time been met consistently in the past? Are the warranty and spare part policies clearly defined? Does it have experience of compliance with international standards and certification? Start Your Evaluation Process with Günay Heat Exchangers With over 40 years of manufacturing experience, Günay Heat Exchangers provides engineering support and technical documentation across a wide product range, from evaporators to condensers, from axial fans to custom-designed heat exchangers. By sharing your project's technical requirements, we can carry out an evaluation together based on the criteria above. To submit your request and speak with our technical team, you can reach us via our contact page. This content was updated on 19 September 2026.
Read More
How Industrial Heat Exchangers Work: A Technical Overview An industrial heat exchanger is a piece of equipment that transfers thermal energy between two fluids that must not mix (one hot, one cold) across a separating surface. The concept looks simple, but choosing the right type of heat exchanger requires serious engineering calculation based on the physical properties of the fluids, operating pressure, temperature difference and the sector in which the application sits. In this article we look at heat exchangers not from a supplier-selection angle but through their working principle and type classification: which heat exchanger works through which physical mechanism, which type is preferred in which sector, and which variables capacity and efficiency depend on. Physical Fundamentals of Heat Transfer To understand the performance of a heat exchanger, you first need to know how heat is transported. Three mechanisms act together in industrial equipment, but the two that dominate heat exchanger design are conduction and convection. Conduction When the hot fluid touches the metal surface of the heat exchanger (a tube wall or plate surface), heat is conducted through the material itself to the opposite surface by molecular vibration. In this step the thermal conductivity of the material (high in copper and aluminum, relatively low in stainless steel) directly determines performance. Convection As the fluid moves along the surface, it picks up heat from the surface or releases heat to it. The velocity, turbulence and viscosity of the fluid are decisive here: in laminar flow the heat transfer coefficient stays low, while in a turbulent flow regime it rises markedly. For this reason plate and fin geometries are deliberately designed to make the flow turbulent. What the Heat Transfer Coefficient (U Value) Means The overall heat transfer coefficient (U) shows how much heat a heat exchanger can transfer per unit of surface area and per unit of temperature difference. The U value is a combination of material thickness and conductivity, the convection coefficient of the fluid on both sides, and the fouling resistance on the surface. In practice, plate heat exchangers generally reach a higher U value than tubular types thanks to the high turbulence they create in narrow channels; this means a smaller surface area and a more compact body for the same heat load. Flow Arrangements: Counterflow and Parallel Flow Another critical parameter that determines heat exchanger performance is the direction of the hot and cold fluids relative to each other. Parallel flow (same-direction flow): Both fluids enter the heat exchanger at the same end and move in the same direction. The temperature difference is high at the inlet but falls rapidly toward the outlet; this lowers the log mean temperature difference (LMTD) and limits total heat transfer. Counterflow (opposite-direction flow): The fluids enter from opposite ends. The temperature difference is distributed more evenly along the heat exchanger and the mean LMTD is higher than in parallel flow. As a result, more heat can be transferred with the same surface area; this is why the vast majority of industrial heat exchangers are designed on the counterflow principle. Crossflow: Seen especially in air-cooled heat exchangers; the airflow passes perpendicular to the fluid in the tube bundle. Fin geometry and tube layout are the main factors that determine efficiency in this arrangement. Heat Exchanger Types and Working Principles There are three main heat exchanger families widely used in industry; each is optimized for different pressure, temperature and fluid conditions. Plate Heat Exchangers Plate heat exchangers are built by stacking thin metal plates stamped with corrugated patterns. The hot and cold fluids pass through alternating channels and exchange heat across the plate surface. The corrugated pattern makes the flow turbulent, which gives a high heat transfer coefficient and a compact body. Sealing can be provided by gaskets (gasketed type) or by brazing (brazed type). Plate heat exchangers are preferred especially in facilities with limited installation space and in applications in the medium pressure/medium temperature range; however, they are at a disadvantage with very high pressures or fluids containing coarse particles, because of the risk of channel clogging. Shell-and-Tube Heat Exchangers These consist of a tube bundle placed inside an outer shell. One fluid flows through the tubes, the other through the shell, between the tubes. Thanks to their structural strength, they are preferred in heavy-industry applications that require high pressure and a large temperature difference (for example steam systems and process heating). They allow easier disassembly for maintenance and cleaning than plate types, which is an advantage in facilities working with fluids prone to fouling. On the other hand, they require a larger volume and weight than plate heat exchangers for the same heat load. Air-Cooled (Finned-Tube) Heat Exchangers In this type, heat transfer takes place between a liquid or gas and air rather than between liquid and liquid. Thin metal fins (usually aluminum) are mounted on the tubes that carry the fluid to increase the heat transfer surface, and a fan moves air across these fin surfaces. Because the heat transfer coefficient of air is low compared with liquids, fin density and fan airflow are the decisive elements of the design. This principle forms the basis of the evaporators and condensers used in refrigeration systems; both types of equipment work with a combination of a finned tube bundle and an axial fan. Evaporators: Heat Absorption Through Evaporation An evaporator works on the principle that a refrigerant evaporating at low pressure draws heat from the ambient air (or from another fluid to be cooled). As the refrigerant changes from liquid to gas inside the finned tube bundle, it absorbs latent heat from its surroundings; compared with sensible heat transfer, this carries far more energy per unit of mass. For this reason, evaporators can reach a higher cooling capacity than sensible-heat exchangers of the same size. In evaporator designs used in cold rooms, industrial cooling tunnels and process cooling lines, the fin spacing directly affects the frequency of frosting (defrost) and therefore system efficiency; in low-temperature applications a wider fin spacing is preferred. Condensers: The Condensation Principle A condenser performs the opposite function to an evaporator: the gaseous refrigerant leaving the compressor at high pressure and temperature rejects its heat to the outside environment (air or water) on the condenser surface, condenses and returns to the liquid state. The latent heat principle applies at this stage as well; a large amount of heat is released as the gas turns into liquid, and this heat must be removed effectively. In air-cooled condensers, the balance between fin surface area, fan airflow and ambient temperature directly determines the condensing pressure and therefore the energy consumption of the compressor. An undersized condenser lowers the efficiency of the entire system. Material Selection: Copper, Aluminum, Stainless Steel The durability of a heat exchanger depends on material selection as much as its thermal performance does. Copper: Frequently preferred as a tube material thanks to its high thermal conductivity; it shows good corrosion resistance especially in refrigerant lines. Its weight and cost are higher than aluminum. Aluminum: Common as a fin material because of its light weight and good thermal conductivity; in finned tube bundles the copper tube–aluminum fin combination is a standard practice in industry. It may need an additional coating in some corrosive environments. Stainless steel: Although its thermal conductivity is lower than that of copper and aluminum, it is preferred in process heat exchangers working with aggressive fluids and in the food sector because of its chemical resistance and its tolerance to high temperature and pressure. Its cleanability is an advantage in applications with high hygiene requirements. Material selection must be evaluated not only for thermal performance but together with corrosion risks such as the chemical composition of the fluid, ambient humidity and salty air (coastal regions). Wrong material selection leads to performance loss in the short term and premature failure in the long term. Choosing the Right Heat Exchanger Type by Sector Refrigeration and Air Conditioning Sector In cold rooms, commercial refrigeration systems and industrial air-conditioning facilities, finned tube evaporators and condensers are the standard solution. In these systems, which are supported by axial fans, the fin spacing is optimized according to the ambient humidity level and the target temperature. Food and Beverage Industry Hygiene and cleanability are the priority; for this reason plate heat exchangers (especially in liquid food pasteurization) and stainless steel surfaces are preferred. The ability to be dismantled and cleaned frequently is decisive with regard to food safety regulations. Chemical and Process Industry When high pressures, corrosive fluids and wide temperature ranges are involved, shell-and-tube heat exchangers stand out. In these facilities, material compatibility (stainless steel, special alloys) can become more critical than thermal performance. Energy and Heavy Industry Large-capacity shell-and-tube heat exchangers stand out in applications that require a high temperature difference, such as steam generation and waste heat recovery; in these facilities structural strength and long service life are a higher priority than compact size. Günay's product family intersects with this field especially in process cooling circuits: dry coolers that reject heat to the ambient air, condensers and finned tube heat exchangers. Steam and high-pressure process lines, on the other hand, require a separate engineering evaluation. Capacity and Efficiency Factors The capacity a heat exchanger delivers in the field may differ from catalog values. The main variables that determine capacity are the following: Surface area and geometry: Fin density, tube diameter and layout, and the plate corrugation pattern all affect the heat transfer surface and turbulence. Flow velocity and flow rate: If the flow drops into the laminar regime at low flow rates, the heat transfer coefficient falls significantly. Temperature difference (ΔT) and flow direction: A counterflow arrangement gives higher efficiency than parallel flow for the same surface area. Material conductivity: Copper and aluminum offer less resistance than stainless steel. Fouling resistance (fouling factor): Sediment, dirt or a layer of frost that builds up on the surface over time creates additional thermal resistance and lowers the U value. Design Approaches for Increasing Efficiency Achieving higher efficiency under the same operating conditions usually comes not from enlarging the physical size of the heat exchanger but from optimizing its geometry. The main approaches used in practice are the following: Increasing surface area: Increasing fin density or the number of tubes enlarges the heat transfer surface; however, since this also increases the pressure drop on the air side, it must be balanced against fan power. Turbulence-promoting geometries: The corrugated pattern in plate heat exchangers, or the internal surface roughness used in tubular types, makes the flow turbulent early and raises the convection coefficient. Optimum tube/fin layout: Placing tube rows in a staggered arrangement gives better mixing and higher heat transfer on the air side than an in-line layout. Choosing the right fluid velocity: Both very low and very high velocities hurt efficiency; at low velocity the flow falls into the laminar regime, while at excessively high velocity the pressure drop and the risk of erosion increase. Fouling and the Effect of Maintenance on Performance Scale, oil, dust or a biological layer that builds up on the heat exchanger surface adds an extra layer of resistance to heat transfer and, over time, leads to a visible drop in capacity. In finned tube heat exchangers, dust build-up and frosting restrict airflow, increasing the energy consumption of the fan while lowering capacity. In shell-and-tube types, scaling on the inner surface has a similar effect. For this reason a periodic cleaning program is an operating cost item that must not be overlooked when selecting a heat exchanger; types that are easy to dismantle and clean (shell-and-tube, gasketed plate) are preferred in applications prone to fouling. What to Consider When Choosing the Right Heat Exchanger When selecting a heat exchanger, the following technical parameters should be evaluated together: Operating temperature range and maximum temperature difference Working pressure and tolerance to pressure fluctuations Chemical composition of the fluids and corrosion risk Installation space and weight constraints Maintenance access and cleaning frequency Long-term operating cost at the expected capacity As a company that has been manufacturing refrigeration and heat transfer equipment for more than 40 years, we have seen in the field many times that these variables are interdependent and that the right choice cannot be made by looking at a single parameter. All the evaporator, condenser, axial fan and heater solutions we have produced throughout our corporate history are sized with this engineering logic. You can reach our entire product range on the products page. Get Technical Support for Your Project The right heat exchanger type and capacity calculation vary with the project's operating temperature, fluid properties and site conditions; instead of a generic recommendation, an assessment based on concrete project data is needed. To discuss the technical requirements of your project with our engineering team, you can reach us through our contact page. This content was updated on September 19, 2026.
Read More
The Right Question in Condenser Selection: Not "Which Brand" but "Which Application" In industrial refrigeration projects, condenser research often starts with the wrong question: "Which manufacturer is better?" Yet the technical correctness of a condenser selection is determined by the application itself before the manufacturer. The condensing load in a cold room, in a supermarket display system and in a chemical process line are subject to the same physical rules, but in practice they call for very different condenser architectures. Rather than comparing suppliers, this article covers how the different condenser types work and which solution is technically more appropriate in which application. The aim is to offer a decision framework that proceeds not from brands or price lists, but from heat load, climate conditions, water infrastructure and maintenance capacity. Air-Cooled Condensers: Working Principle and Areas of Use In an air-cooled condenser, the refrigerant arriving from the compressor as superheated vapor releases its heat to the air stream passing over it as it flows through the finned tube bundle, and condenses. The air stream is usually forced by one or more axial fans. The system's performance depends directly on three variables: fin surface area, air velocity and the outdoor dry-bulb temperature. Advantages It requires no water consumption; it offers an operating advantage in regions with water scarcity or high water costs. Maintenance items tied to the water circuit, such as scaling, Legionella risk and water treatment costs, are eliminated. Installation and commissioning are relatively simple, and no additional equipment such as a water pump or cooling tower is needed. Limitations In air-cooled systems the condensing temperature runs above the ambient temperature by a certain approach difference. In summer, especially in regions that see high outdoor temperatures, this means an increase in compressor head pressure and therefore in energy consumption. In high-capacity facilities or those operating under continuous load, this is a factor that must be considered at the very start of sizing. Water-Cooled Condensers: For Applications Requiring High Capacity In water-cooled condensers, heat transfer takes place between the refrigerant and circulating water; the water that has absorbed the heat is then released to the atmosphere in a cooling tower or an open/closed-circuit cooler. Because the heat-carrying capacity of water is markedly higher than that of air, the same heat load can be handled with a much more compact heat exchanger surface. Shell-and-Tube Type The most common configuration in industrial facilities is the shell-and-tube type, in which the refrigerant condenses on the shell side and the water circulates inside the tube bundle. This design offers advantages such as resistance to high pressure, compact layout and the ability to remove and clean the tube bundle; for this reason it is a preferred choice in industrial plants with continuous production. Water Consumption and Water Quality Requirements The most critical operating constraint of water-cooled systems is water quality. If hardness, dissolved solids content and pH are not kept under control, scaling (fouling) forms on the inner surface of the tubes; this lowers the heat transfer coefficient and raises the condensing pressure. For this reason, the decision to move to a water-cooled condenser must be evaluated not only through capacity calculation, but also on whether the facility has water treatment and chemical dosing infrastructure. Evaporative Condensers: Hybrid Efficiency An evaporative condenser works like a synthesis of air-cooled and water-cooled systems: water is sprayed over the tube bundle while an air stream is passed through with a fan at the same time. As the water evaporates, it draws heat from the refrigerant in the tubes; this allows the condensing temperature to run close to the wet-bulb temperature, which is much lower than the dry-bulb temperature. The result is a lower head pressure and less compressor energy than an air-cooled system, and lower water consumption than a water-cooled system. This type is preferred especially in ammonia industrial refrigeration systems and high-capacity cold storage facilities; however, it requires additional maintenance items such as a water circulation pump, a drift eliminator and periodic water blowdown. Condenser Selection by Application Condenser type selection should be made according to the facility's operating conditions rather than a theoretical efficiency ranking. The three examples below show how the same question is answered differently in different applications. Cold Rooms In large-volume cold rooms, the load profile is usually long-lasting and relatively constant; the outdoor temperature fluctuates seasonally. In these facilities, air-cooled condensers are a common choice because they need no water circuit and have low operating complexity; in hot-climate regions, sizing the fin surface and fan group accordingly can noticeably reduce summer energy consumption. Supermarket and Retail Refrigeration Systems In supermarket display and storage refrigeration systems, space constraints, noise level and maintenance accessibility are the priority criteria. In this segment, compact air-cooled condenser blocks suitable for rooftop or exterior-wall mounting are mostly the better solution in terms of both investment cost and ease of maintenance. Systems that require a water circuit create an additional maintenance burden in businesses such as supermarkets that have no technical staff. Industrial Facilities and Process Cooling In industrial applications that require continuous, high-capacity loads, such as chemicals, food processing or process cooling, water-cooled shell-and-tube condensers stand out. These facilities usually already have a cooling tower or a process water line; this infrastructure makes the additional cost of a water-cooled system worthwhile. In addition, tight-tolerance temperature control in process lines benefits from the more stable condensing pressure offered by water-cooled systems. Capacity Calculation Logic: What It Is Sized By Condenser sizing is not an arbitrary choice of size but the result of a specific calculation chain. The general logic works as follows: Total heat rejection load: The heat the condenser must reject is the sum of the cooling load absorbed in the evaporator and the compression heat the compressor adds to the refrigerant. In other words, condenser capacity is always chosen larger than evaporator capacity. Design approach temperature (approach/TD): The condenser is sized according to the difference between a specified condensing temperature and the ambient temperature (dry-bulb for air-cooled, wet-bulb for evaporative, inlet water temperature for water-cooled). As this difference gets smaller, the heat exchanger surface gets larger, but operating efficiency increases. Heat transfer surface and coefficient: Fin spacing, tube diameter, material conductivity and fluid velocity determine the amount of heat that can be transferred per unit of surface. A fouling factor is always included in the calculation, especially in water-cooled systems. Air/water flow rate: Fan or pump flow rate is chosen to deliver the required heat transfer; insufficient flow raises the condensing pressure, while excessive flow leads to unnecessary energy consumption and, in some cases, increased noise. Each of these steps leads to a meaningful sizing when evaluated not on a fixed cooling load but on the facility's real operating scenario (part load, summer/winter difference, units running simultaneously). The nominal capacity values in catalogs are only a starting reference; the final selection must be verified against the facility's actual operating conditions. Especially in facilities with multi-shift production or seasonal load fluctuations, evaluating the condenser not only for peak load but also for the medium-load condition seen most often during the year reflects the real operating cost more accurately. Condenser–Fan Compatibility: The Overlooked Part of System Integrity In air-cooled and evaporative condensers, most of the performance is determined as much by the fan group accompanying the condenser as by the condenser body itself. Insufficient airflow or a wrongly chosen fan pressure curve makes even the best-designed condenser surface inefficient. The blade angle, speed and flow-versus-static-pressure curve of axial fans must be chosen to match the condenser's fin density and air resistance. A common mistake in practice is sizing the condenser body correctly but leaving the fan selection to a standard catalog; this causes the expected capacity not to be reached in the field. For this reason, condenser and fan selection must be treated not independently of each other but as a single thermal system. Factors That Determine Energy Efficiency A condenser's energy performance depends not on a single number but on the combined effect of several factors: The difference between condensing temperature and ambient temperature: The lower this difference can be kept, the lower the compressor head pressure and the higher the compressor efficiency. Fin/tube surface cleanliness: Dust, an oil film or scaling directly lowers the heat transfer coefficient; the difference in energy consumption between a clean surface and a fouled one is quickly felt in operation. Fan control strategy: Using speed-controlled fans (EC motors or frequency inverters) instead of fixed-speed fans can provide noticeable energy savings under part load and low outdoor temperature conditions. Material and fin geometry: While a copper tube–aluminum fin combination is sufficient for general-purpose applications, in corrosive environments copper-nickel or coated surfaces protect both service life and long-term efficiency. None of these factors is decisive on its own; correct condenser selection requires these variables to be optimized together according to the facility's operating profile. Maintenance Requirements and Condenser Life The condenser type directly determines the maintenance regime. In air-cooled systems, maintenance comes down largely to periodic cleaning of the fin surface and checking the fan motor/bearings, whereas in water-cooled systems water quality monitoring, chemical dosing and periodic tube bundle cleaning are mandatory. In evaporative condensers, the water basin, drift eliminator and spray nozzles also need regular inspection in addition to these. Neglected maintenance does not only increase energy consumption; a compressor that runs continuously at high head pressure because of a fouled surface can wear out earlier than expected. For this reason, when selecting a condenser, the facility's maintenance capacity (technical staff, water treatment infrastructure, ease of access) should also be part of the decision process — a solution that looks the most efficient on paper will not deliver the expected performance in the field if it cannot be maintained. How to Decide on the Right Condenser Solution Condenser selection should be approached as an engineering problem, not a supplier comparison. In the decision process, the following questions should be answered in order: What are the facility's heat rejection load and operating profile? What are the region's climate conditions (dry-bulb/wet-bulb temperatures)? Is there a water source and water treatment infrastructure? What complexity of system can the facility's maintenance capacity support? Are there noise, space or aesthetic constraints? The answers to these questions are largely decisive in determining the condenser architecture (fin density, fan group, capacity step) that best suits the facility. Günay Heat Exchangers' more than 40 years of manufacturing experience offers this evaluation not as abstract theory but as engineering practice verified with field data. The air-cooled condenser, evaporator, axial fan and heater solutions in our product portfolio are designed not as independent components but as parts of a single thermal system; you can find more information about this approach on our corporate page. Let's Determine the Right Condenser Solution for Your Project Together Every facility's heat load, climate conditions and maintenance capacity are different; for this reason the "best condenser" comes not from a single product but from the right engineering assessment. To determine the air-cooled condenser architecture (cabinet type, capacity step, fan configuration) that fits your needs for a cold room, supermarket refrigeration system or industrial process line, contact our team. By evaluating your facility's heat rejection load, existing infrastructure and operating conditions together, let us determine a solution that works in the field, not just on paper. This content was updated on September 17, 2026.
Read More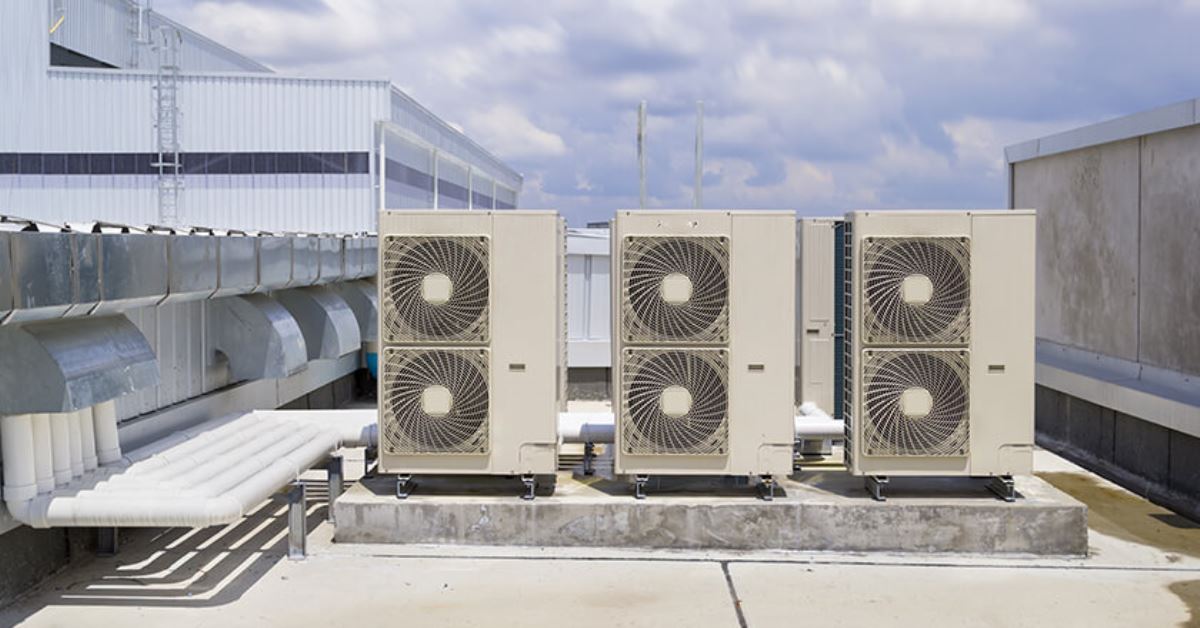
The Purchasing Perspective in Condenser Supply: Why Price, Stock and Lead Time Are Decisive Choosing a condenser correctly from a technical standpoint is only one side of the job. For purchasing teams the real question is usually different: when will this product be in my hands, at what order quantity does the price advantage begin, is there an alternative waiting in stock, or is custom production needed? For OEM companies planning production in the refrigeration and air-conditioning sector, for plant investors and for maintenance-repair teams, condenser supply is as much a matter of timing and cost planning as it is an engineering decision. In this article we cover the questions the purchasing side should ask when evaluating a condenser supplier, the variables that determine pricing, and how the delivery process works. Delivery from Stock or Custom Production? The Basic Distinction The first decision point in condenser supply is whether the requirement can be met with a standard model. Air-cooled condensers produced in standard capacity ranges may be held in the warehouse in certain sizes, depending on the supplier's stock policy, and in that case the lead time is shortened considerably. On the other hand, when there is a special airflow, a special casing size, compatibility with a different refrigerant or a project-specific installation requirement, the order enters the production line and the timeline changes completely. The most practical thing to do on the purchasing side is to clarify this distinction at the inquiry stage: asking early "Is there stock at this capacity, or will we enter the production plan?" prevents surprise delays in the quotation process. At this point the capacity and type variety of the condenser product group directly affects supplier selection; manufacturers with a wide model range increase the likelihood of meeting the demand from stock. When Can It Be Met from Stock? Delivery from stock may be possible for standard capacities, commonly used types and frequently requested sizes. This is generally the preferred route for spare part needs, urgent replacements after a failure or small-scale projects. When Is Custom Production Required? Custom production is unavoidable in project-based plant installations, special airflow/pressure requirements, different material requests (for example a stainless steel casing) or applications requiring OEM integration. In this case the lead time extends depending on design approval and production capacity. How Does Minimum Order Quantity (MOQ) Work in Condenser Supply? In industrial equipment supply, the concept of minimum order quantity is not applied as strictly as with consumer products, but it still directly affects pricing logic. A unit cost difference arises between a single condenser order and a multi-unit order of the same model and capacity; the reason is that the fixed costs of production line setup time, material procurement logistics and quality control processes are spread over the order quantity. For OEM manufacturers and dealers who buy in bulk, this turns into a concrete advantage: buyers who commit to predictable annual or quarterly volumes can obtain better terms in both price and production priority by signing a framework agreement with the supplier. The point purchasing teams should watch here is not to confuse "minimum order" with "economic order quantity." The former refers to the lower limit the supplier accepts, and the latter to the quantity at which the buyer strikes the best cost-benefit balance. For companies doing long-term supply planning, the second concept is far more decisive. Factors That Determine Pricing Condenser pricing is made up not of a single item but of several interrelated variables. When comparing quotations, having these items visible separately allows a genuine comparison between suppliers. Material and Capacity The casing material (galvanized, aluminum, stainless steel), the tube-fin configuration and the capacity range form the basis of the price. Materials chosen for higher corrosion resistance or for special environmental conditions increase cost, but can reduce maintenance and replacement frequency in the long run. Quantity and Bulk Purchase Discounts In connection with the MOQ logic mentioned above, an improvement in unit price is expected as volume increases. This discount rate varies from supplier to supplier and is generally proportional to the duration of the order commitment (one-off or an annual framework agreement). Degree of Customization Deviation from a standard model — special connection points, a different fan configuration, special painting/coating — is reflected in the price because it requires engineering time and production line adjustment. As the customization request becomes clearer, the quotation process also speeds up; unclear or changing specifications lead to repeated revisions and therefore delays. OEM Cooperation Models For OEM companies that manufacture refrigeration equipment, condenser supply is usually not a one-off purchase but an ongoing production partnership. The form of this relationship directly affects supply cost and flexibility. Standard Product Integration The OEM company integrates the supplier's catalog condenser directly into its own final product (refrigeration unit, chiller, split system, etc.). This model is the fastest option with the most predictable cost; lead times shorten depending on stock status. Build-to-Spec Production The condenser is produced according to the OEM company's own technical specification. In this model, a mutual technical verification process is carried out with the supplier's engineering team; parameters such as dimensions, connection type and performance curve are clarified at the start of the project. Although the process takes longer, it provides full compatibility with the OEM's own product line. Long-Term Framework Agreements OEMs that request a certain volume at regular intervals gain both price stability and production priority by signing an annual or multi-year framework agreement with the supplier. This model gives the OEM side predictability against fluctuations in the supply chain. OEMs that also source product groups other than condensers (evaporator, axial fan, heater, heat exchanger) from the same supplier can gain additional efficiency by managing logistics and quality control processes from a single hand. Delivery Process: From Order Confirmation to Shipment Although the lead time in condenser supply is expressed as a single figure, in the background a process made up of several stages runs. Knowing these stages allows the purchasing side to make realistic time planning. 1. Technical Approval and Specification Clarification Before ordering, the capacity, connection type, installation direction and any special conditions (ambient temperature, fluid type) are clarified. Uncertainty at this stage is the most frequent cause of delays in the process. 2. Production Planning The order is scheduled according to the current workload of the production line. For products that can be met from stock this stage is skipped or very short; in custom production the duration varies with material procurement and line capacity. 3. Production and Quality Control After production is completed, pressure testing, leak-tightness checking and performance verification are carried out. This stage is a safety and quality step that must not be skipped; a supplier that shortens these checks with the promise of fast delivery should not be preferred. 4. Shipment and Export Logistics Road transport is standard for domestic deliveries; for export orders, customs documents, suitable packaging and the transport mode (land/sea) are added to the time. Working with a supplier that focuses on export shortens the process because these steps have become routine. The list of countries exported to is a concrete indicator of a supplier's cross-border shipping experience; manufacturers that export regularly cause fewer surprises in customs and logistics processes. Stock Management: Critical Spare Parts and Urgent Needs For production facilities and refrigeration system operators, an urgent condenser need caused by a failure requires a different approach from planned purchasing. In such cases the supplier's stock depth and availability of common models become decisive. Businesses that want to reduce the risk of production stoppage on critical equipment can agree on a stock guarantee or a priority production arrangement by discussing their frequently used capacity ranges with the supplier in advance. This is a method that improves the cost-risk balance especially for facilities with a maintenance-repair contract. What Do Warranty and After-Sales Service Mean? Another topic as important as price and lead time is how after-sales responsibility is shared. Which failures the warranty covers, for how long and under which conditions; how quickly spare parts are supplied; how technical support requests are managed — all of these affect the total cost of ownership. A supplier with a low unit price but weak warranty and service support can lead to higher cost in the long run. In the purchasing process, it is recommended that quotation comparison be made not only on product price but also on warranty period, service accessibility and spare part supply speed. When making this evaluation, looking not at the price of a single order but at the total cost the equipment will generate over its operating life gives a healthier picture. Whether a spare part can be obtained within weeks or from stock on the same day in the event of a failure is directly related to the cost of production downtime. For this reason, purchasing teams should add warranty period and service response speed as an item in the quotation evaluation table. Questions to Ask When Comparing the Right Supplier Is the capacity I am requesting in stock, or does it enter the production plan? How does the price change with bulk purchases or a framework agreement? How does the custom-specification production process work, and how many revisions are allowed? To which standards are quality control and testing carried out? Who manages the customs and logistics process in export orders? What is the warranty coverage and the spare part supply time? Is priority production or a stock guarantee offered for urgent/failure-related requests? Being able to get clear answers to these questions gives an idea not only of the supplier's product quality but also of its process maturity. Working with manufacturers that have been producing in the sector for more than forty years and whose corporate history is transparent increases the likelihood of getting consistent answers to such questions. Günay Heat Exchangers' corporate history and production capacity can be examined as a reference point in such an evaluation process. Additional Factors in Export-Oriented Supply For companies that ship equipment abroad or manufacture for the DACH/European market, condenser supply has one more layer: compliance with the target country's technical standards (CE marking, material certification), multilingual technical documentation, and communication speed due to time zone/language differences. At this point a supplier with export experience reduces the risk of surprise delays, because it has turned customs procedures and international freight bookings into a routine workflow. The concrete proof of such experience is the number and variety of countries the supplier actually exports to. Choose the Right Partner in Condenser Supply Supply decisions made without evaluating price, stock status and lead time together can turn into cost or time losses in later stages of the project. The right approach is to clarify your requirement (whether it will be met from stock or with custom production), your volume (single order or framework agreement) and your after-sales expectations (warranty, service, spare parts), and to compare along these three axes. If you would like a concrete quotation on capacity, lead time and pricing for your condenser needs, you can share the details of your project by getting in touch with our team. When you submit your request, you receive a quotation with clear information on stock status, production time and bulk purchase terms; you can submit your quotation request through our contact page. This content was updated on September 15, 2026.
Read More
Why a "One-Size-Fits-All" Solution Does Not Work in Industrial Refrigeration Systems The cooling need of a food processing plant and that of a data center rest on the same physical principles (evaporation, condensation, heat transfer), yet from an engineering standpoint they are completely different. On one side, temperature must be brought down within seconds for product safety; on the other, the priority is to operate year-round without interruption within a narrow temperature band. This is where the work of the engineer who builds the refrigeration system begins: not choosing components such as evaporators, condensers, axial fans and heaters from a catalog and lining them up side by side, but analyzing the application's load, ambient conditions and operating rhythm and bringing these components together in the right capacity and configuration. Instead of redefining refrigeration system components, this article looks at how these components are sized differently in four sectors — food processing, cold storage/logistics, pharmaceutical-chemical industry and data centers — and which design decisions come into play. The aim is to answer not "which product is better" but "which combination and sizing is right for this application." The Backbone of the System: How the Role of the Four Components Changes by Sector The same four components sit at the heart of every industrial refrigeration system, but their size, material and control logic change from application to application. An evaporator with the same nominal capacity in two different facilities behaves completely differently when installed with a different airflow direction, a different defrost frequency and a different fin spacing. For this reason, evaluating component selection independently of the application's heat load profile and ambient conditions is one of the most common mistakes leading to unexpected efficiency losses in the field. Evaporators: Where the Heat Load Is Met Evaporators are the component that draws heat from the environment or the product; however, while a freezing tunnel aims for high heat transfer within seconds, a storage room aims for a long-term low and constant temperature. This difference directly affects design parameters such as fin spacing, number of fans and defrost frequency. Condensers: Managing the Rejected Heat Condensers reject the heat drawn from the system to the outside environment. In facilities where the ambient temperature is high or the condenser is placed in a closed or poorly ventilated mechanical room, condenser capacity must be selected with a safety margin above the standard values in manufacturers' catalogs; otherwise system efficiency drops noticeably in the summer months. Axial Fans: Designing Air Circulation Axial fans provide the airflow on both the evaporator and the condenser side; however, airflow velocity and volume differ greatly by application. For example, in delicate food products where direct airflow onto the product is undesirable, low-speed, wide-volume fans are preferred, while in applications requiring fast cooling, high airflow takes priority. Heaters: Preventing Freezing and Ice Build-Up Heaters are used during defrost operations and to prevent icing in drain pans and drain lines operating at low temperatures. The defrost strategy (hot gas, electric or water defrost) varies by sector; in cold rooms with frequent door traffic, defrost frequency is much higher than in pharmaceutical storage. Refrigeration System Design in Food Processing Plants In food processing lines, the job of the refrigeration system is not only to cool the product but to move product safety through the critical temperature range (generally the band in which microbial growth accelerates) as quickly as possible. In meat, dairy and ready-meal production, "blast chilling" lines require a combination of high-capacity evaporators and high-airflow fans until the core temperature drops to a certain level. System Design Logic in Food Processing In food plants, design is based on product load (mass, initial temperature, target temperature) and line speed. During intensive production hours the heat load peaks in a short time; for this reason evaporator capacity is sized not for the average but for the peak load. In addition, because of hygiene requirements, fin and casing designs with stainless surfaces that are easy to clean are preferred. Fan placement also varies by product type: for unpackaged products processed in the open, direct airflow onto the product may be undesirable, in which case ducted air distribution is preferred; for packaged products, more aggressive air circulation shortens the cooling time. Challenges Encountered in Food Processing Increased moisture load and frosting risk caused by frequent door openings and personnel traffic Different product groups (raw meat, cooked product, frozen product) requiring different temperature zones in the same facility Scheduling cleaning (CIP) cycles without interrupting the continuity of system operation Refrigeration System Design in Cold Storage and Logistics In storage and logistics facilities, the priority is not rapid temperature reduction as in food processing lines, but maintaining a constant temperature over a long period in a large-volume space with low energy use. Here, system design is shaped by storage volume, insulation quality, rack layout (whether it obstructs air circulation) and especially door/dock traffic. System Design Logic in Cold Storage In multi-chamber cold rooms, each chamber may serve a different product group (frozen, chilled, controlled atmosphere), so evaporator and condenser selection is made separately for each chamber. Since heat gain is higher in areas near shipping docks, additional capacity margin is provided for these areas. On the condenser side, where many refrigeration circuits are connected to a common mechanical yard, condenser capacity needs to be planned centrally so as to cover the total simultaneous load. Challenges Encountered in Cold Storage Hot/humid air ingress through doors that are constantly opened by forklift and personnel traffic Ensuring temperature uniformity in large-volume spaces (rack shadows, dead zones in airflow) The high share of energy cost in total operating expense due to 24/7 operation Precise Temperature Control in the Pharmaceutical and Chemical Industry In pharmaceutical storage, active ingredient production and some chemical processes, the temperature tolerance is far narrower than in food and logistics applications. The real engineering question here is not "how fast can we cool" but "how narrow a band, and how reliably, can we hold the temperature." System Design Logic in Pharma and Chemicals In this sector systems are generally installed redundantly: having one refrigeration circuit take over when the other fails is a standard approach so that a temperature deviation does not lead to the loss of critical product. In chemical processes, there may also be situations where gases or vapors in the environment cause corrosion on components, so the material selection of evaporators and condensers (coating, casing material) is evaluated according to the environment's chemistry. Control systems are also designed to work integrated with continuous monitoring and alarm logic. Challenges Encountered in Pharma and Chemicals Even small deviations leading to product loss or quality problems because of the narrow temperature tolerance Low tolerance for interruption, and therefore the need for redundant systems and alarm infrastructure Corrosive environmental conditions in some processes affecting component life Data Centers: The Heat Rejection Side and the Role of Condensers and Dry Coolers Data centers are a different category that must remove a continuous and intense electronic heat load rather than cool a product. In these facilities, indoor cooling is generally provided by air handling units and chiller systems; Günay's products come into play on the heat rejection side of these systems, that is, in outdoor units such as condensers and dry coolers. The heat load in server rooms is largely constant and interruption is unacceptable; for this reason heat rejection equipment must be sized to suit continuous operation. Heat Rejection Side Design Logic in Data Centers On the heat rejection side of these facilities, axial fan selection is critical; because the balance of airflow and static pressure must be optimized according to the placement and air resistance of the condenser or dry cooler. Being able to use outdoor air during periods when climate conditions are suitable (free cooling potential) is a design parameter evaluated for energy efficiency in dry cooler and heat exchanger based solutions. In such projects the overall cooling architecture is determined by the data center's main design; the heat rejection equipment is sized according to the data of that design. Challenges Encountered in Data Centers Component reliability coming to the fore because of the requirement for uninterrupted operation Preventing hot air recirculation in equipment placement Maintaining heat rejection capacity even at high outdoor temperatures in the summer months Energy Efficiency Priorities That Vary by Sector Energy efficiency matters in every sector; however, the definition of an "efficient system" is not fixed — it is shaped by the application's operating profile, and what is being optimized changes with that profile. In cold rooms the priority is to reduce compressor and fan running hours under a continuous, large-volume load; for this reason variable-speed fan control and evaporator designs that can operate efficiently at part load stand out. In food processing lines, energy efficiency is generally achieved by not oversizing the system for peak load moments, that is, by selecting capacity that suits the real production profile. In the pharmaceutical and chemical sector, the redundancy priority can sometimes override energy efficiency; a second circuit is kept continuously ready for reliability. On the heat rejection side of data centers, using outdoor air seasonally and correctly matching the fan/condenser are among the design decisions that make the biggest difference in total energy consumption. The Engineering Process for the Right System Design Whatever the sector, a reliable refrigeration system design follows a certain order. First the heat load is calculated; this calculation includes not only the heat from the product or equipment but also heat gains from building insulation, lighting, personnel density and door/dock traffic. Then evaporator and condenser capacity is determined according to this total load; here not only the nominal capacity but also the seasonal variation of the ambient temperature is taken into account. Fan selection is made according to airflow, noise level and static pressure constraints — especially in enclosed spaces, duct resistance directly affects fan performance. Finally, the defrost and freeze-prevention strategy, including the use of heaters, is planned according to the operational rhythm: in a facility with frequent door openings the defrost cycle is triggered at shorter intervals, while in a closed, low-traffic storage room less frequent defrost may be sufficient. Passing any of these steps with a standard template, without taking into account the real operating conditions of the sector, causes the system either to fall short or to consume more energy than necessary. Why an Application-Specific Engineering Approach Makes a Difference There is no shortage of suppliers offering a wide product range on the market; the real difference emerges in how these products are brought together according to the load profile, ambient conditions and operating rhythm of a specific application. A wide catalog does not replace the right engineering decision — what matters is which evaporator is matched with which condenser, which fan airflow and which defrost strategy. As a manufacturer that has been in the refrigeration sector for more than 40 years, Günay Heat Exchangers treats evaporator, condenser, axial fan and heater components not as ready-made packages selected from catalogs but as a system sized according to each project's heat load and operating conditions. By accessing detailed information about our product range, you can assess which component combination your project needs. Get Technical Support for Your Project Whether it is food processing, cold storage, pharmaceutical-chemical production or a data center, every application has its own heat load and operating condition. The Günay Heat Exchangers engineering team can help you determine the right combination of evaporator, condenser, axial fan and heater by evaluating your project's requirements. To size your system correctly and build energy efficiency into the design from the start, talk to our team. This content was updated on September 11, 2026.
Read More
For most purchasing teams, choosing a refrigeration system supplier begins with the question "which product works better?" Yet once the project kicks in, the truly critical question is different: will this supplier be able to deliver on the date promised, at the capacity promised, under the conditions promised? Product selection is a technical matter; supplier selection is a supply chain and risk management decision. Especially in export projects, multi-stage assembly lines or investments tied to a commissioning schedule, the wrong supplier choice can delay the whole project regardless of product quality. In this article we focus not on product features but on the criteria that actually decide the purchasing process: delivery processes, stock and production capacity, scope of technical support, export/logistics experience, quality control steps and contract terms. Why Is Supplier Selection a Supply Chain Decision? When buying an evaporator or condenser, the technical specification can usually be clarified; capacity, refrigerant type and size limits are already defined in the project documents. What remains uncertain is when the product will reach you, via which logistics route and under which commitment. For this reason, professional purchasing teams apply a second filter after completing the technical evaluation: the operational reliability of the supplier. This filter covers delivery performance history, production capacity, stock policy and export experience. Lead Time: The First and Most Tangible Evaluation Criterion The question to ask about lead time is not "how long does it take" but "how is this time guaranteed". For standard stock products the lead time is usually clear; for custom-designed equipment the time may vary because production planning, material procurement and testing processes come into play. A serious supplier clarifies this distinction at the start of the project and offers two separate delivery schedules at the quotation stage. The Difference Between Standard Products and Custom Designs While standard condenser or evaporator models can be supplied from stock or with a short production cycle, orders requiring special airflow, special material (for example a stainless steel housing) or project-specific connection dimensions follow a longer process because of engineering approval, material procurement and production sequence. When evaluating a supplier, ask for a separate delivery commitment for these two scenarios; a single general lead time promise is generally not realistic. Reflecting the Delivery Commitment in the Contract A verbal delivery promise does not protect the project. The quotation and order confirmation document should state in writing the delivery date, possible revision scenarios (for example delay in technical approval, change in the payment plan) and how the date will be updated in these scenarios. A supplier showing this transparency at the quotation stage is also an indication of how well it controls its own production planning. Stock and Production Capacity: Preparing for Demand Fluctuations In the cooling sector demand is seasonal; order volume rises as summer approaches and relatively calms down in winter months. How a supplier manages this fluctuation directly affects the delivery security of your project. A supplier whose production line is planned only according to its own utilisation rate may cause unexpected delays when you enter the order queue in a busy period. Critical Component and Spare Part Stock Whether the supplier keeps frequently failing or replaceable components such as fan motors, control boards and expansion valves in stock must definitely be asked before purchase. Obtaining these components from abroad or from a third-party supplier every time is a hidden risk that prolongs the response time in case of failure. Production Line Flexibility A manufacturer that can arrange extra shifts, a parallel production line or prioritisation when demand increases can maintain its delivery commitment in a crisis. The practical way to understand this capacity is to ask the supplier for concrete information about its current order load and typical delivery window; vague or evasive answers are usually a sign of a capacity limit. Technical Support and After-Sales Service Capacity The process that begins after the equipment is delivered is the real test of supplier selection. Commissioning support, response speed in case of failure and the completeness of technical documentation directly affect long-term operating cost. Commissioning (Installation) Support Evaporators, condensers and other cooling equipment often work integrated with other systems on site (compressor, control panel, piping). Whether the supplier offers technical personnel support during commissioning and provides the site team with documents for installation and parameter settings are concrete criteria that reduce the risk of failure in the first months of the project. Fault Response Process and Spare Part Access Is the communication channel to the supplier clear at the time of a fault? Can the technical team provide remote support and, when needed, send personnel to the site? Through which process are spare part requests met? The answers to these questions should be clarified before the contract; the support policy after the warranty period ends should also be asked about separately, because many suppliers do not give details on this at the quotation stage. Technical Documentation and Spare Part Catalogue Whether documents such as the installation manual, electrical diagram, maintenance intervals and spare parts list are provided completely with the delivery is a practical criterion that prevents loss of time during operation. If this documentation is missing, your site team remains dependent on the supplier for every small question; this is a serious source of delay especially for export customers working in different time zones. The languages in which the documentation is provided should also be asked about separately in international projects. Export Experience and International Logistics Competence When choosing a supplier for projects abroad, familiarity with customs processes, international transport coordination and the technical/documentation requirements of the target market is decisive as much as product quality. A manufacturer without export experience, even if it makes the right product, can slow the project down on matters such as CE documentation, packaging standards or transport insurance. Günay Heat Exchangers' experience of regular shipments to the DACH region and the European market shows that customs and logistics processes can be planned according to the project schedule; the countries it exports to indicate the geographic scope of this experience. When evaluating a supplier, questioning this history with concrete references is a much more reliable indicator than the statement "we can export". Quality Control Processes: From Production to Shipment When and how quality control is carried out determines whether the product will work without problems on site. Concrete information about this process should be requested from the supplier before purchase; the general statement "we comply with quality standards" is not sufficient. Control Points During Production At which stage of production critical points such as weld quality, tube-fin joint tightness and housing leak-tightness are checked must be clarified. In a production that performs quality control only at the final test, without intermediate control steps, the risk of not detecting a faulty part early increases. Final Inspection Before Shipment The criteria with which final-stage checks such as pressure testing, leak-tightness checking and visual inspection are performed before shipment should, if possible, be documented with a written inspection report. In export projects this report prevents disputes that may arise at customs or during acceptance. Points to Watch in Contract and Warranty Terms As much as the technical specification, the commercial clauses of the contract also determine supplier risk. What the warranty scope includes and excludes, the conditions to be applied in case of delay and how the payment plan matches the delivery stages should be clarified in writing before starting the project. Warranty Scope and Duration In addition to the warranty period, which types of faults the scope covers (material defect, workmanship defect, performance deviation) and which situations fall outside the warranty (incorrect installation, unsuitable operating conditions) should be clearly defined in the contract. Vague warranty clauses lead the parties to make different interpretations at the time of a fault. Delivery Delay and Performance Conditions Having in the contract the conditions to be applied if the delivery date is exceeded (revised delivery plan, notification obligation) is also a sign of how seriously the supplier takes its delivery commitment. A supplier hesitating to accept these clauses may not fully trust its own capacity planning. Matching the Payment Plan to the Delivery Stages Linking the payment schedule to concrete stages such as production approval, intermediate inspection, shipment and installation balances the risk for both parties. Payment structures that are entirely in advance or entirely after delivery leave one of the parties under unnecessary risk; a staged payment structure functions as a mechanism that mutually confirms the progress of the project and creates a reference point in possible disputes. Not Price, but Total Cost of Supply The supplier offering the lowest unit price is often not the cheapest option. When the downtime cost of a delivery delay, the production loss of the fault response time and the effect of a delay in spare part supply on maintenance cost are taken into account, a supplier with a slightly higher unit price but strong delivery and support assurance may be lower in cost overall. Comparing suppliers not only on the quotation price but also including the cost of these operational risks shows the maturity level of the purchasing decision. Breadth and Technical Depth of the Product Portfolio Instead of a supplier specialised in a single product group, a supplier that produces complementary product groups such as evaporators, condensers, axial fans and heaters under the same roof can offer an advantage in terms of system integrity. Such a supplier can test compatibility between components in advance with its own engineering team and reduce the risk of incompatibility in site integration. Günay Heat Exchangers' product portfolio can be cited as an example of this approach; especially in the condenser line, the different capacity and configuration options may make it possible to provide a single-source solution to project-based supply needs. Corporate Background and Reference Check How many years a supplier has been in operation, which sectors it serves and which projects it has taken part in show whether there is a real operational infrastructure behind its delivery and support promises. A manufacturer with a history of over 40 years in the industry has been tested not in a single large order but in long-term supply relationships. In the supplier evaluation process, getting information about corporate background and production infrastructure is as important a step as the technical quotation; decisions made without asking about reference projects and the current customer portfolio usually carry the risk of surprises. Supplier Evaluation Checklist The topics purchasing teams should concretely ask about during quotation evaluation can be summarised as follows: Is there a separate written delivery commitment for standard products and custom designs? Are critical spare parts kept in stock, and what is the lead time? How is production capacity flexed when demand increases? Are commissioning support and site technical personnel provided? What is the technical support policy after the warranty? Who manages the customs and documentation process in export shipments? Which quality control steps are applied before production and shipment, and are these steps reported? Are delivery delay and warranty scope defined as clear clauses in the contract? Does the payment plan match the delivery stages (production approval, shipment, installation)? Can reference projects and the current customer portfolio be verified? Clarify the Process Now with the Right Supplier The real assurance in refrigeration system supply is not the technical values in the catalogue but that delivery, support and contract terms are concrete and written. To evaluate your project's technical requirements, delivery schedule and export/logistics conditions together, get in touch with the Günay Heat Exchangers team; by passing your request to our technical team you can proceed on the basis of a concrete delivery and support plan. This content was updated on 9 September 2026.
Read More
Fill out the form to discover the most suitable high-end products for your projects. Contact Us Now.
Fairs
Strong Connections Through Fair Participation
Hostech 2025
This year, Hostech by TUSİD 2025 was held on May 27–31 at the Istanbul TÜYAP Fair and Congress Center. As Turkey’s largest and Europe’s second largest HORECA fair, it welcomed approximately 35,000 visitors from 140 countries across a 45,000 m⊃2; exhibition area. Günay Soğutma proudly took part in this major event. At our booth, we showcased our innovative industrial cooling products and sustainable solutions, while also connecting with professionals from both Turkey and abroad. For us, Hostech was more than just a fair; it was a valuable opportunity to build new business partnerships, strengthen existing relationships, and represent our company more powerfully in the international market. The strong interest from foreign buyer delegations once again proved that we are on the right track. We sincerely thank all our visitors and look forward to meeting again at upcoming fairs.
Read More
Chillventa 2022
Thank You to Everyone Who Joined Us at Chillventa 2022! We would like to extend our heartfelt thanks to all participants and valued customers who visited our stand at Chillventa 2022. Your interest and the time you shared with us were a tremendous source of motivation, allowing us to present our innovative cooling solutions and share our vision within the industry. The connections we have built with you strengthen our leadership goals and inspire us to provide more efficient and sustainable solutions in the future. We look forward to building new projects and strong partnerships together!
Read More
Chillventa 2024
Günay Soğutma participated in the Chillventa 2024 Fair, seizing the opportunity to showcase the latest innovations in the sector. During the event, we shared our newest technologies and solutions in the field of cooling and air conditioning with attendees. The fair served as an important platform to connect with industry professionals and foster new collaborations. Visitors had the chance to explore our innovative products and sustainable solutions while gaining insight into our customer-oriented approach. Chillventa 2024 provided not only an opportunity for knowledge exchange but also a chance to keep up with the latest industry trends. We are pleased to have established new business connections and strengthened existing relationships through this experience. We would like to extend our gratitude to all the visitors who joined us at the fair. We eagerly look forward to meeting you again at future events!
Read More
HVAC-R Egypt Expo 2024
With the solutions we presented at HVAC-R EGYPT EXPO, we reinforced our reliability and sustainability principles in the refrigeration and heat transfer sector in Egypt.
Read More
HVAC-R London 2023
HVAC Refrigeration Live, as an important event in the industry, offered a very valuable experience for us. We would like to express our sincere thanks to all exhibitors and customers who visited our booth for their interest and time. The strong ties we have established with you give us great motivation to maintain our leadership in the industry and to carry our solution-oriented approach even further.
Read More
ISK-SODEX Istanbul 2023
We participated in ISK-SODEX 2023, one of the leading exhibitions of the air conditioning industry. We would like to thank all our customers and exhibitors who showed great interest in our stand.
Read More
AquaTherm Exhibition 2023
Thank you to all our customers and exhibitors who visited our booth at AquaTherm Exhibition 2023. Your intense interest made us very happy and we were proud to share our innovations in the sector.
Read More
C&R Madrid 2023
The C&R Madrid 2023 fair was an unforgettable experience for us as an important event in the industry. We extend our heartfelt thanks to all participants and customers who visited our stand for their interest and time. The connections we established with you inspire us to continue our leadership in the industry and strengthen our solution-oriented approach. We look forward to building a more efficient and sustainable future togethe
Read More Gallery
Strong And Reliable Since 1986
dynamic energy of the future
